HZS120 Configuration
A fourth bin creates another independently stored aggregate fraction for the plant layout.
HZS120 is rated at 120 m³/h theoretically and uses a JS2000 mixer. The table introduces four 20 m³ aggregate compartments at this point in the belt-fed range.
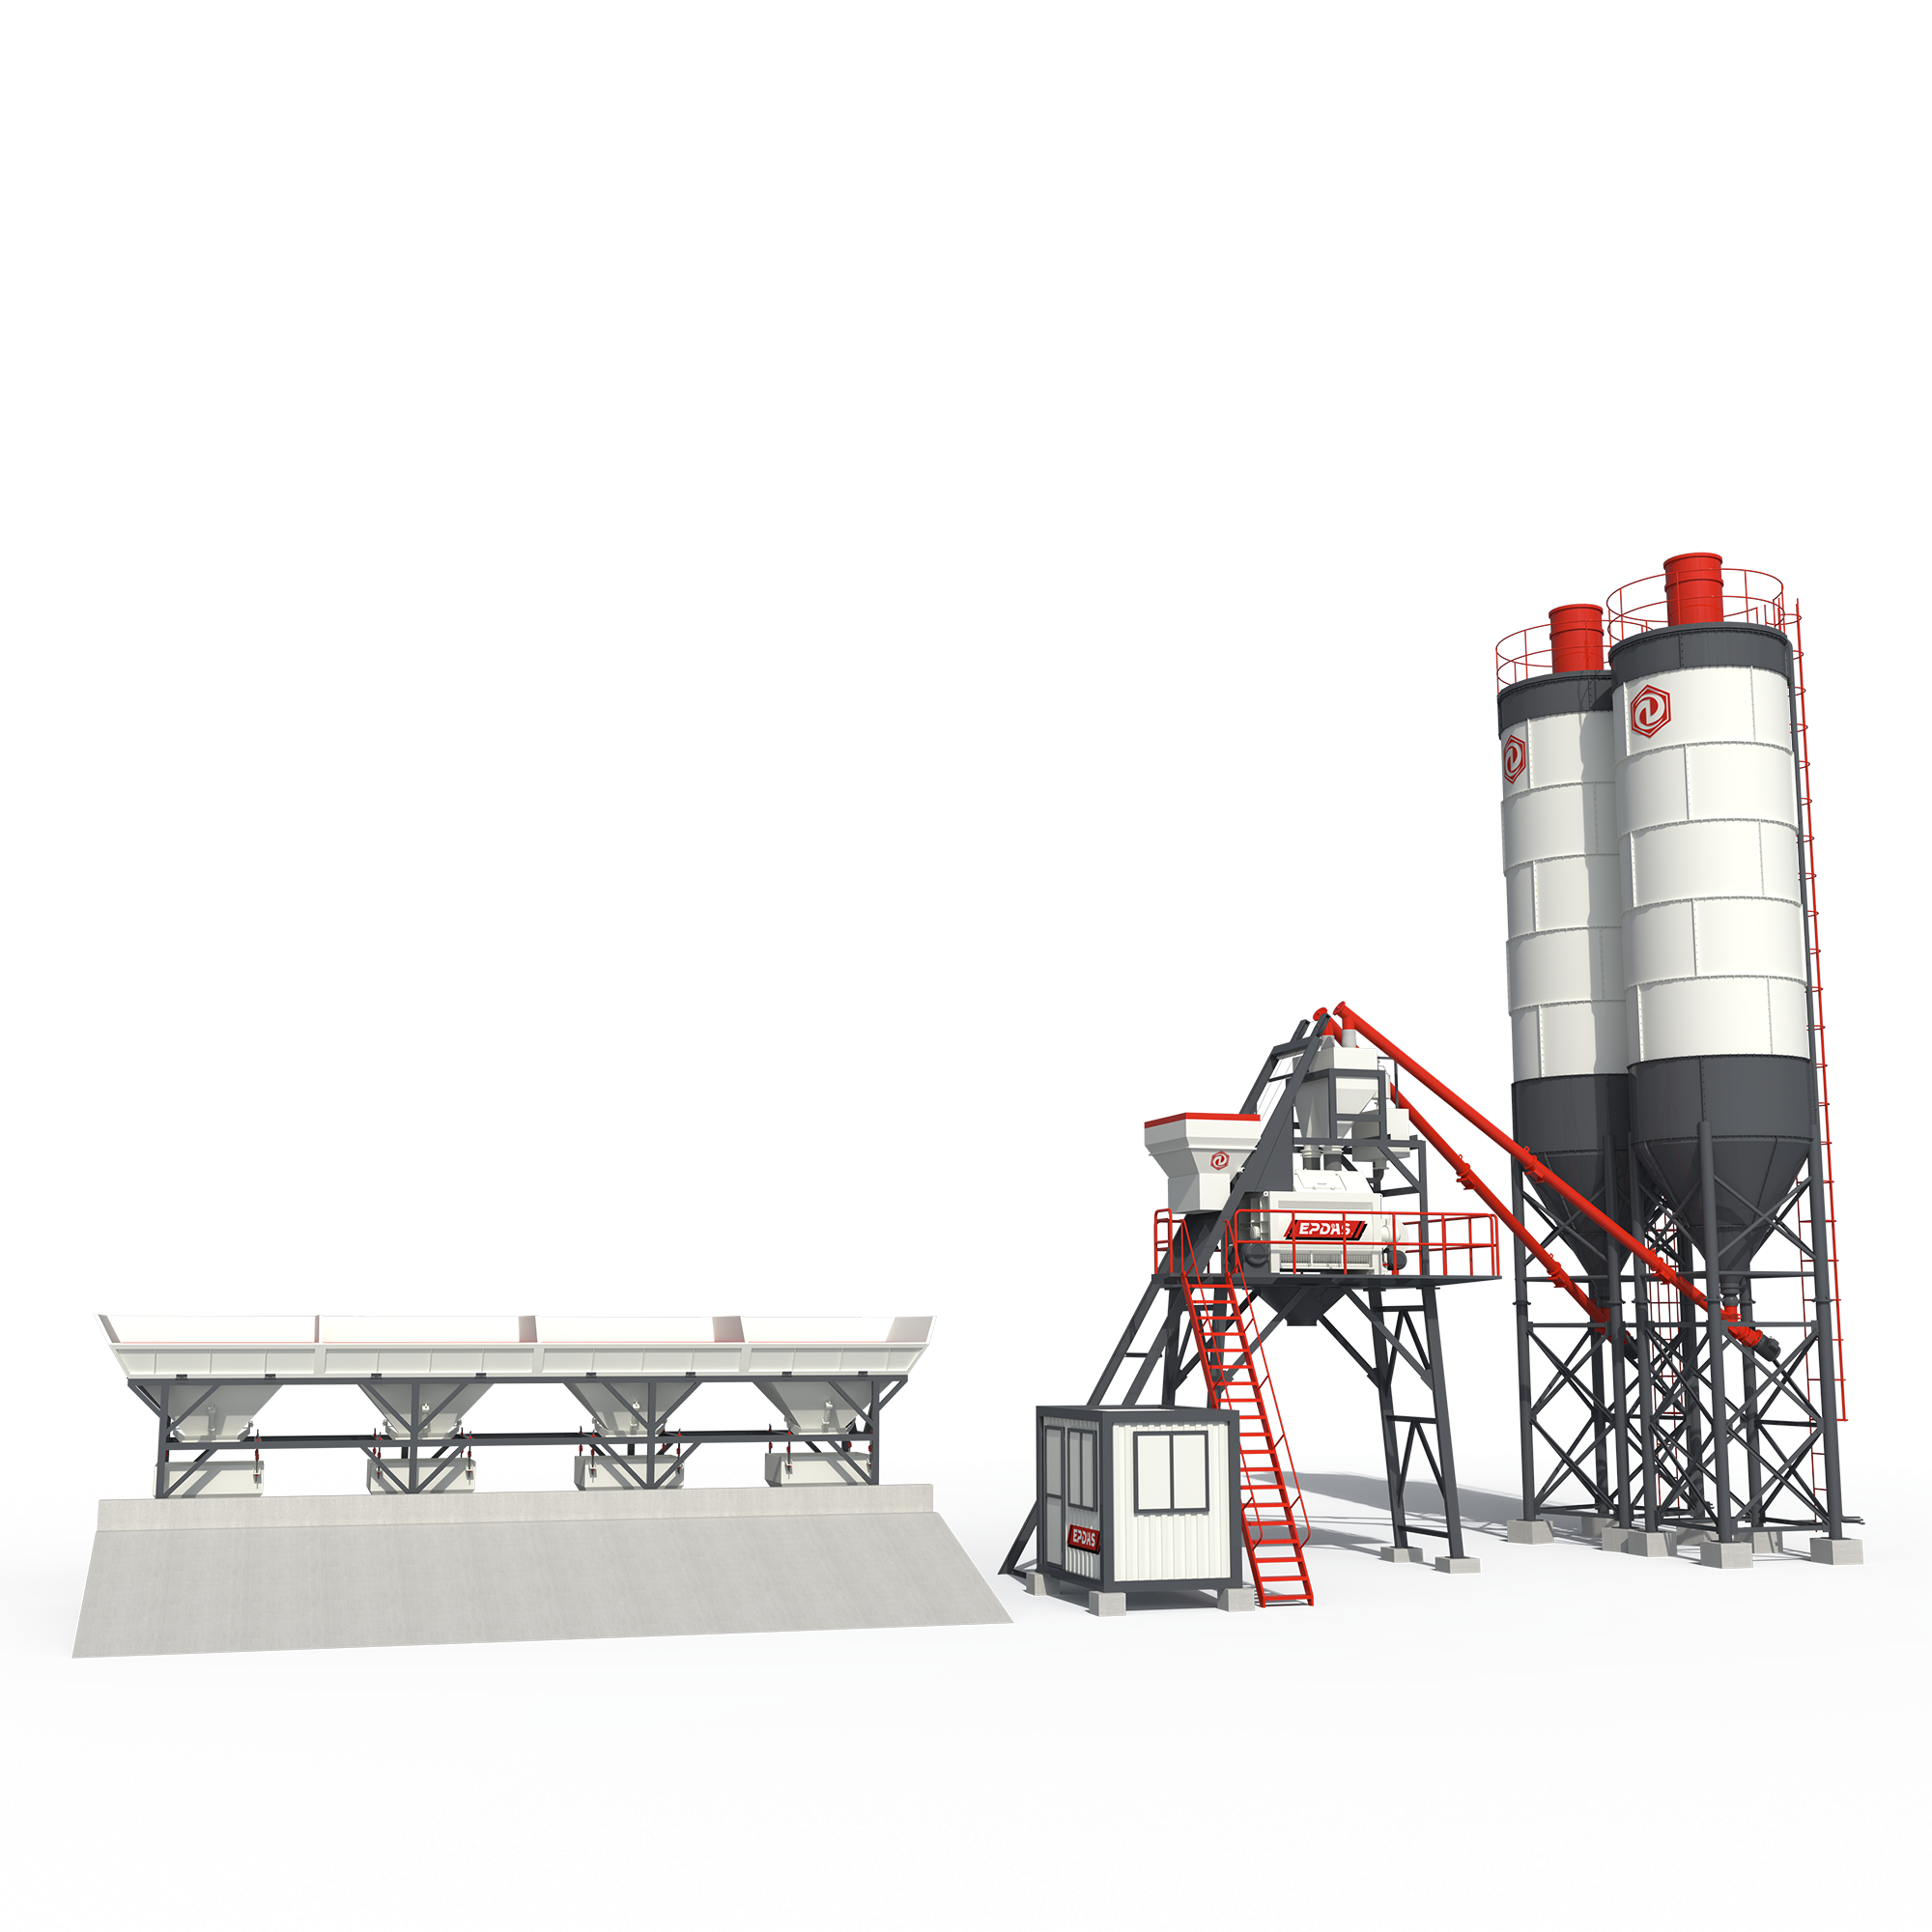
Series rendering. Confirm HZS120's appearance and included equipment in its proposal.
HZS120 centrally mixes weighed ingredients in a JS2000 mixer. Its published 120 m³/h theoretical class combines belt feeding with four 20 m³ aggregate compartments.
Consider a regular ready-mix supply operation needing four independently stored aggregate fractions before moving to the JS3000 class. The receiving fleet and recipe cycle determine usable production.
A fourth bin creates another independently stored aggregate fraction for the plant layout.
Two 37 kW mixing motors accompany the JS2000 configuration.
Understand the role of each connection before building the equipment package.
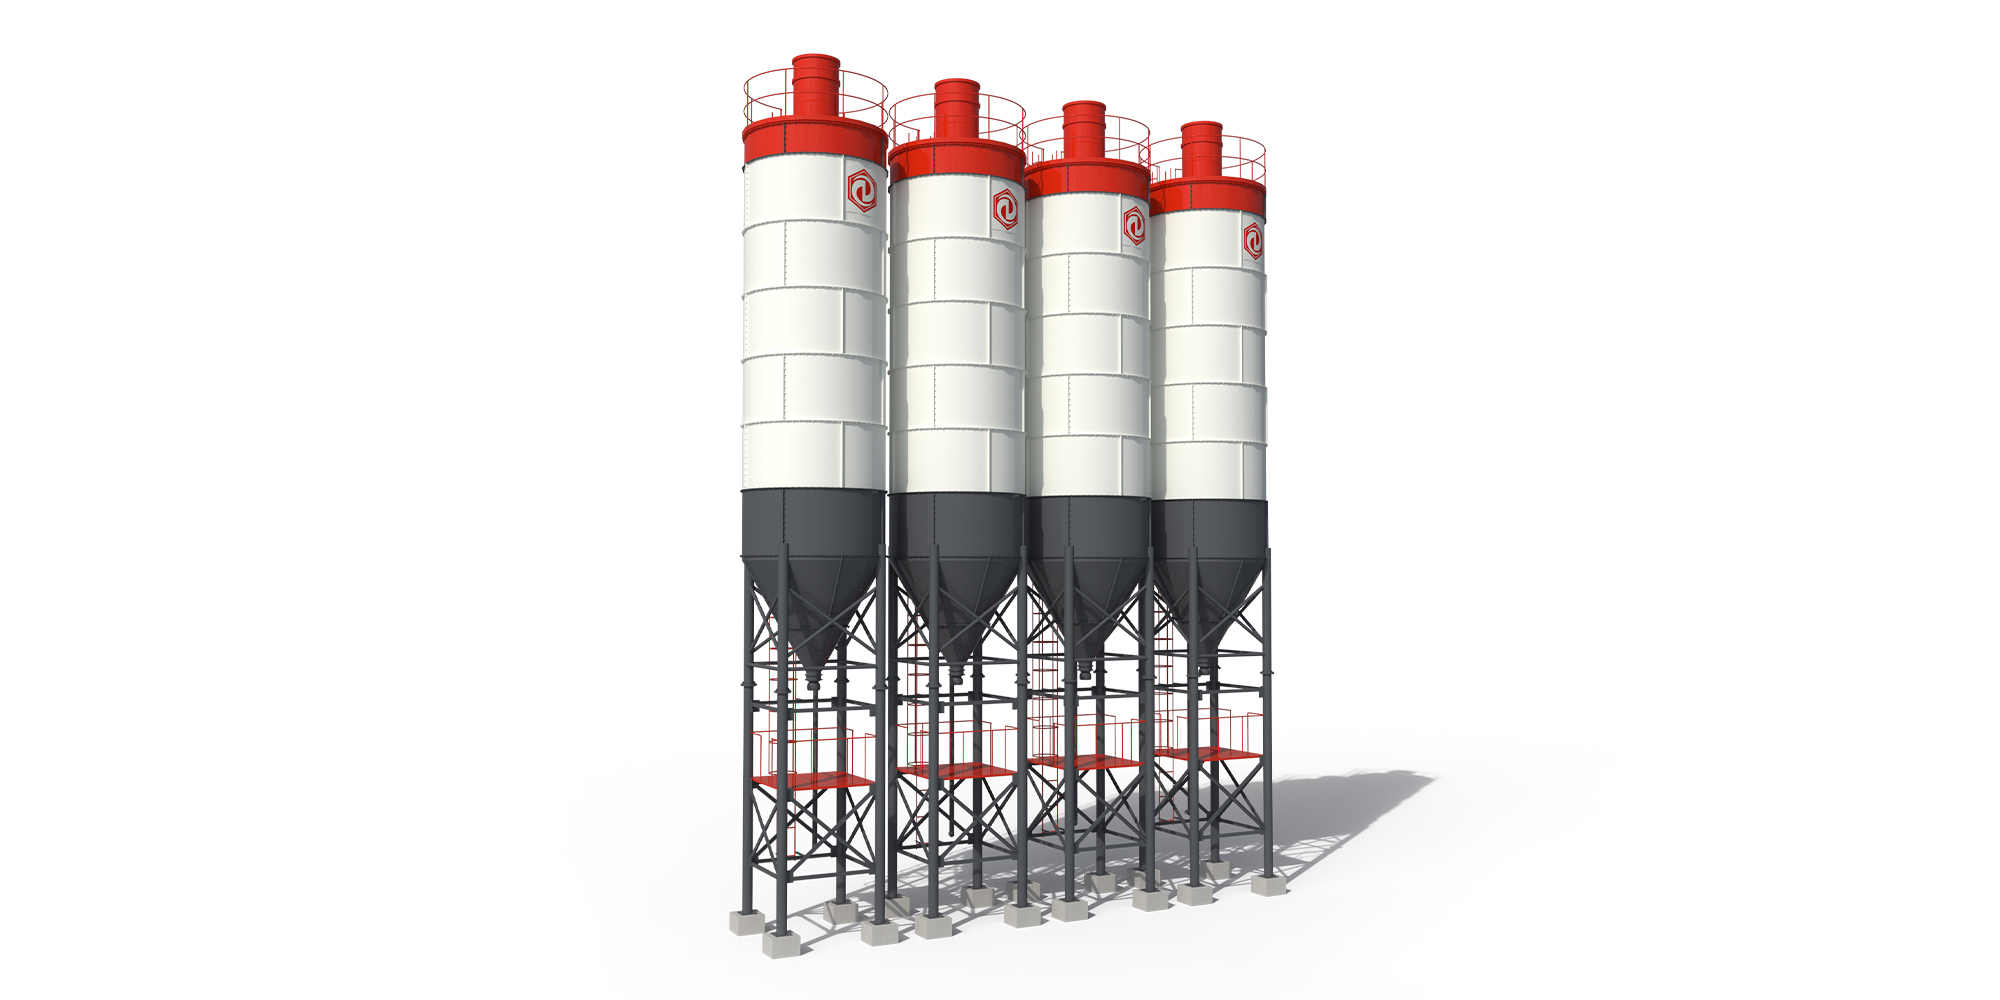 INTERFACE 01 / Cement Silo
Powder storage supports the batching schedule through a separately sized cement inventory.
Calculate usable stock from the intended mixes and replenishment interval, rather than deriving silo size from the model number.
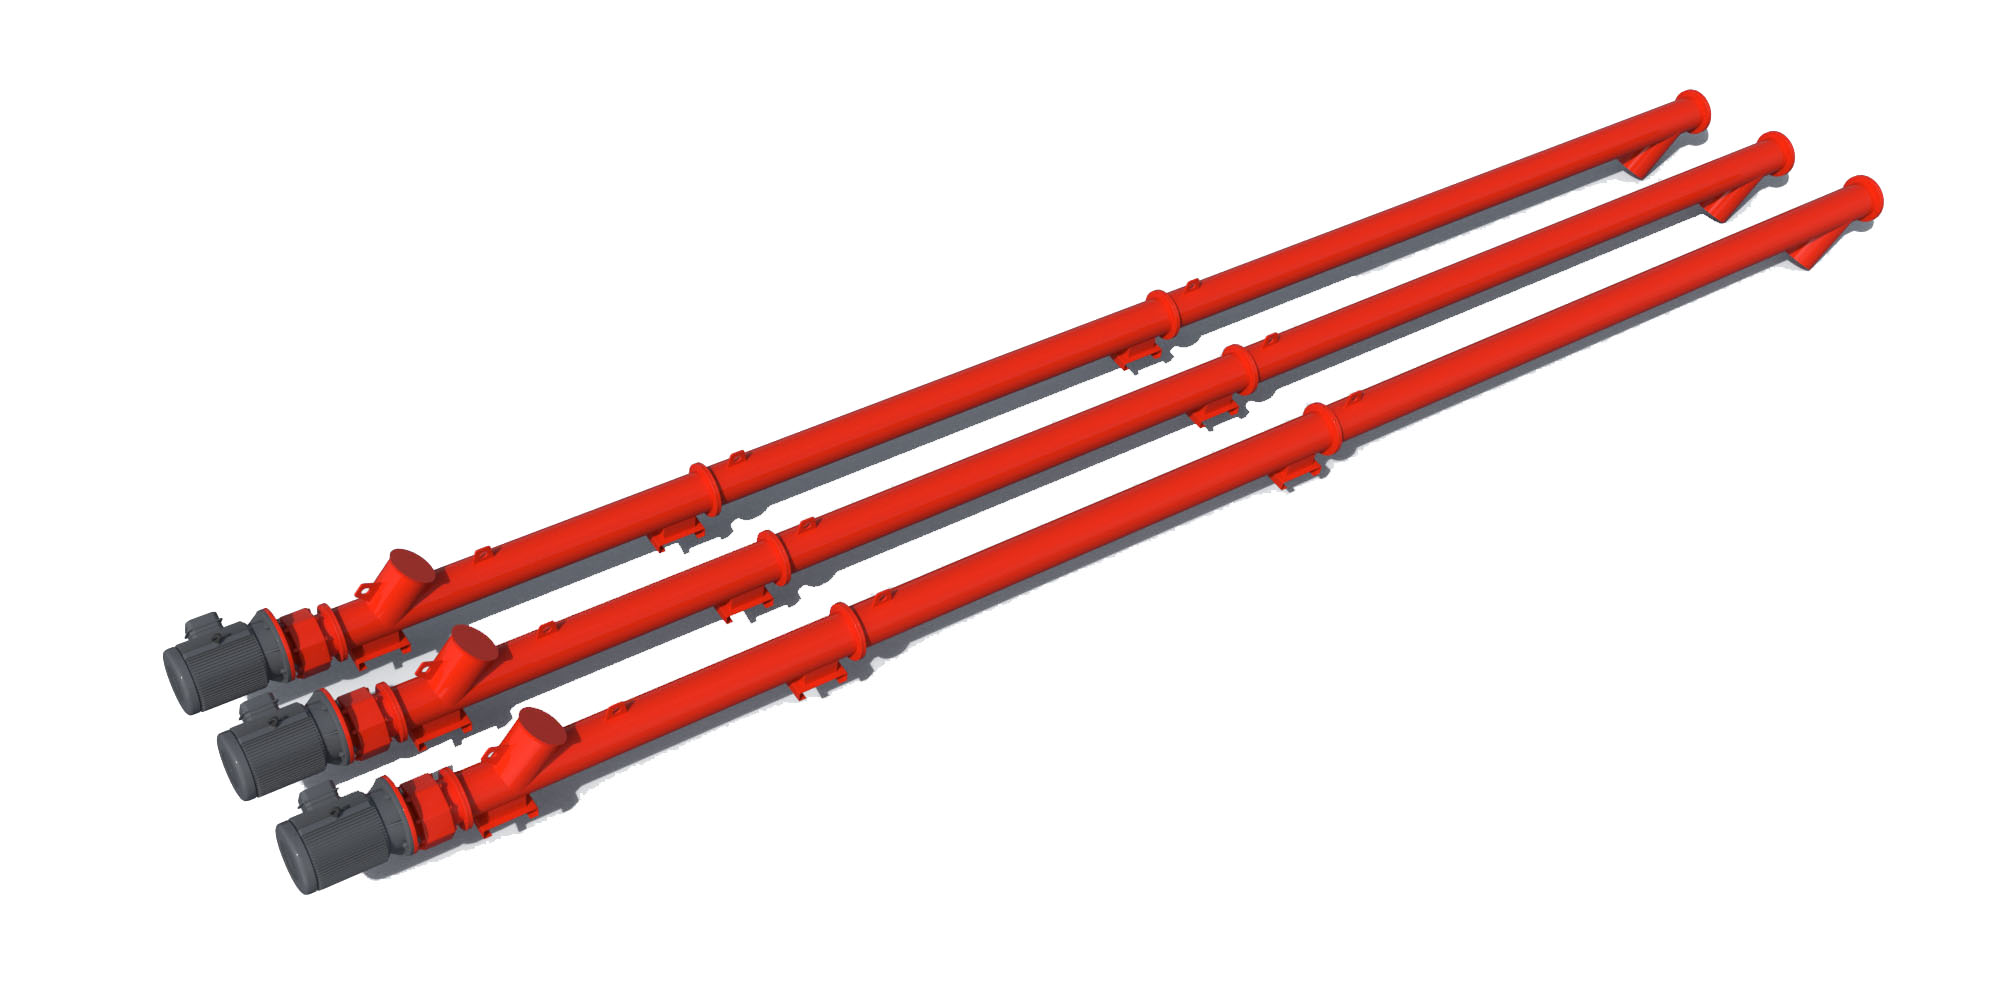 INTERFACE 02 / Screw Conveyor
The powder conveyor connects the selected silo outlet to the plant weighing arrangement.
Review the actual feed time required within the listed 60-second cycle reference; confirm the final conveyor geometry.
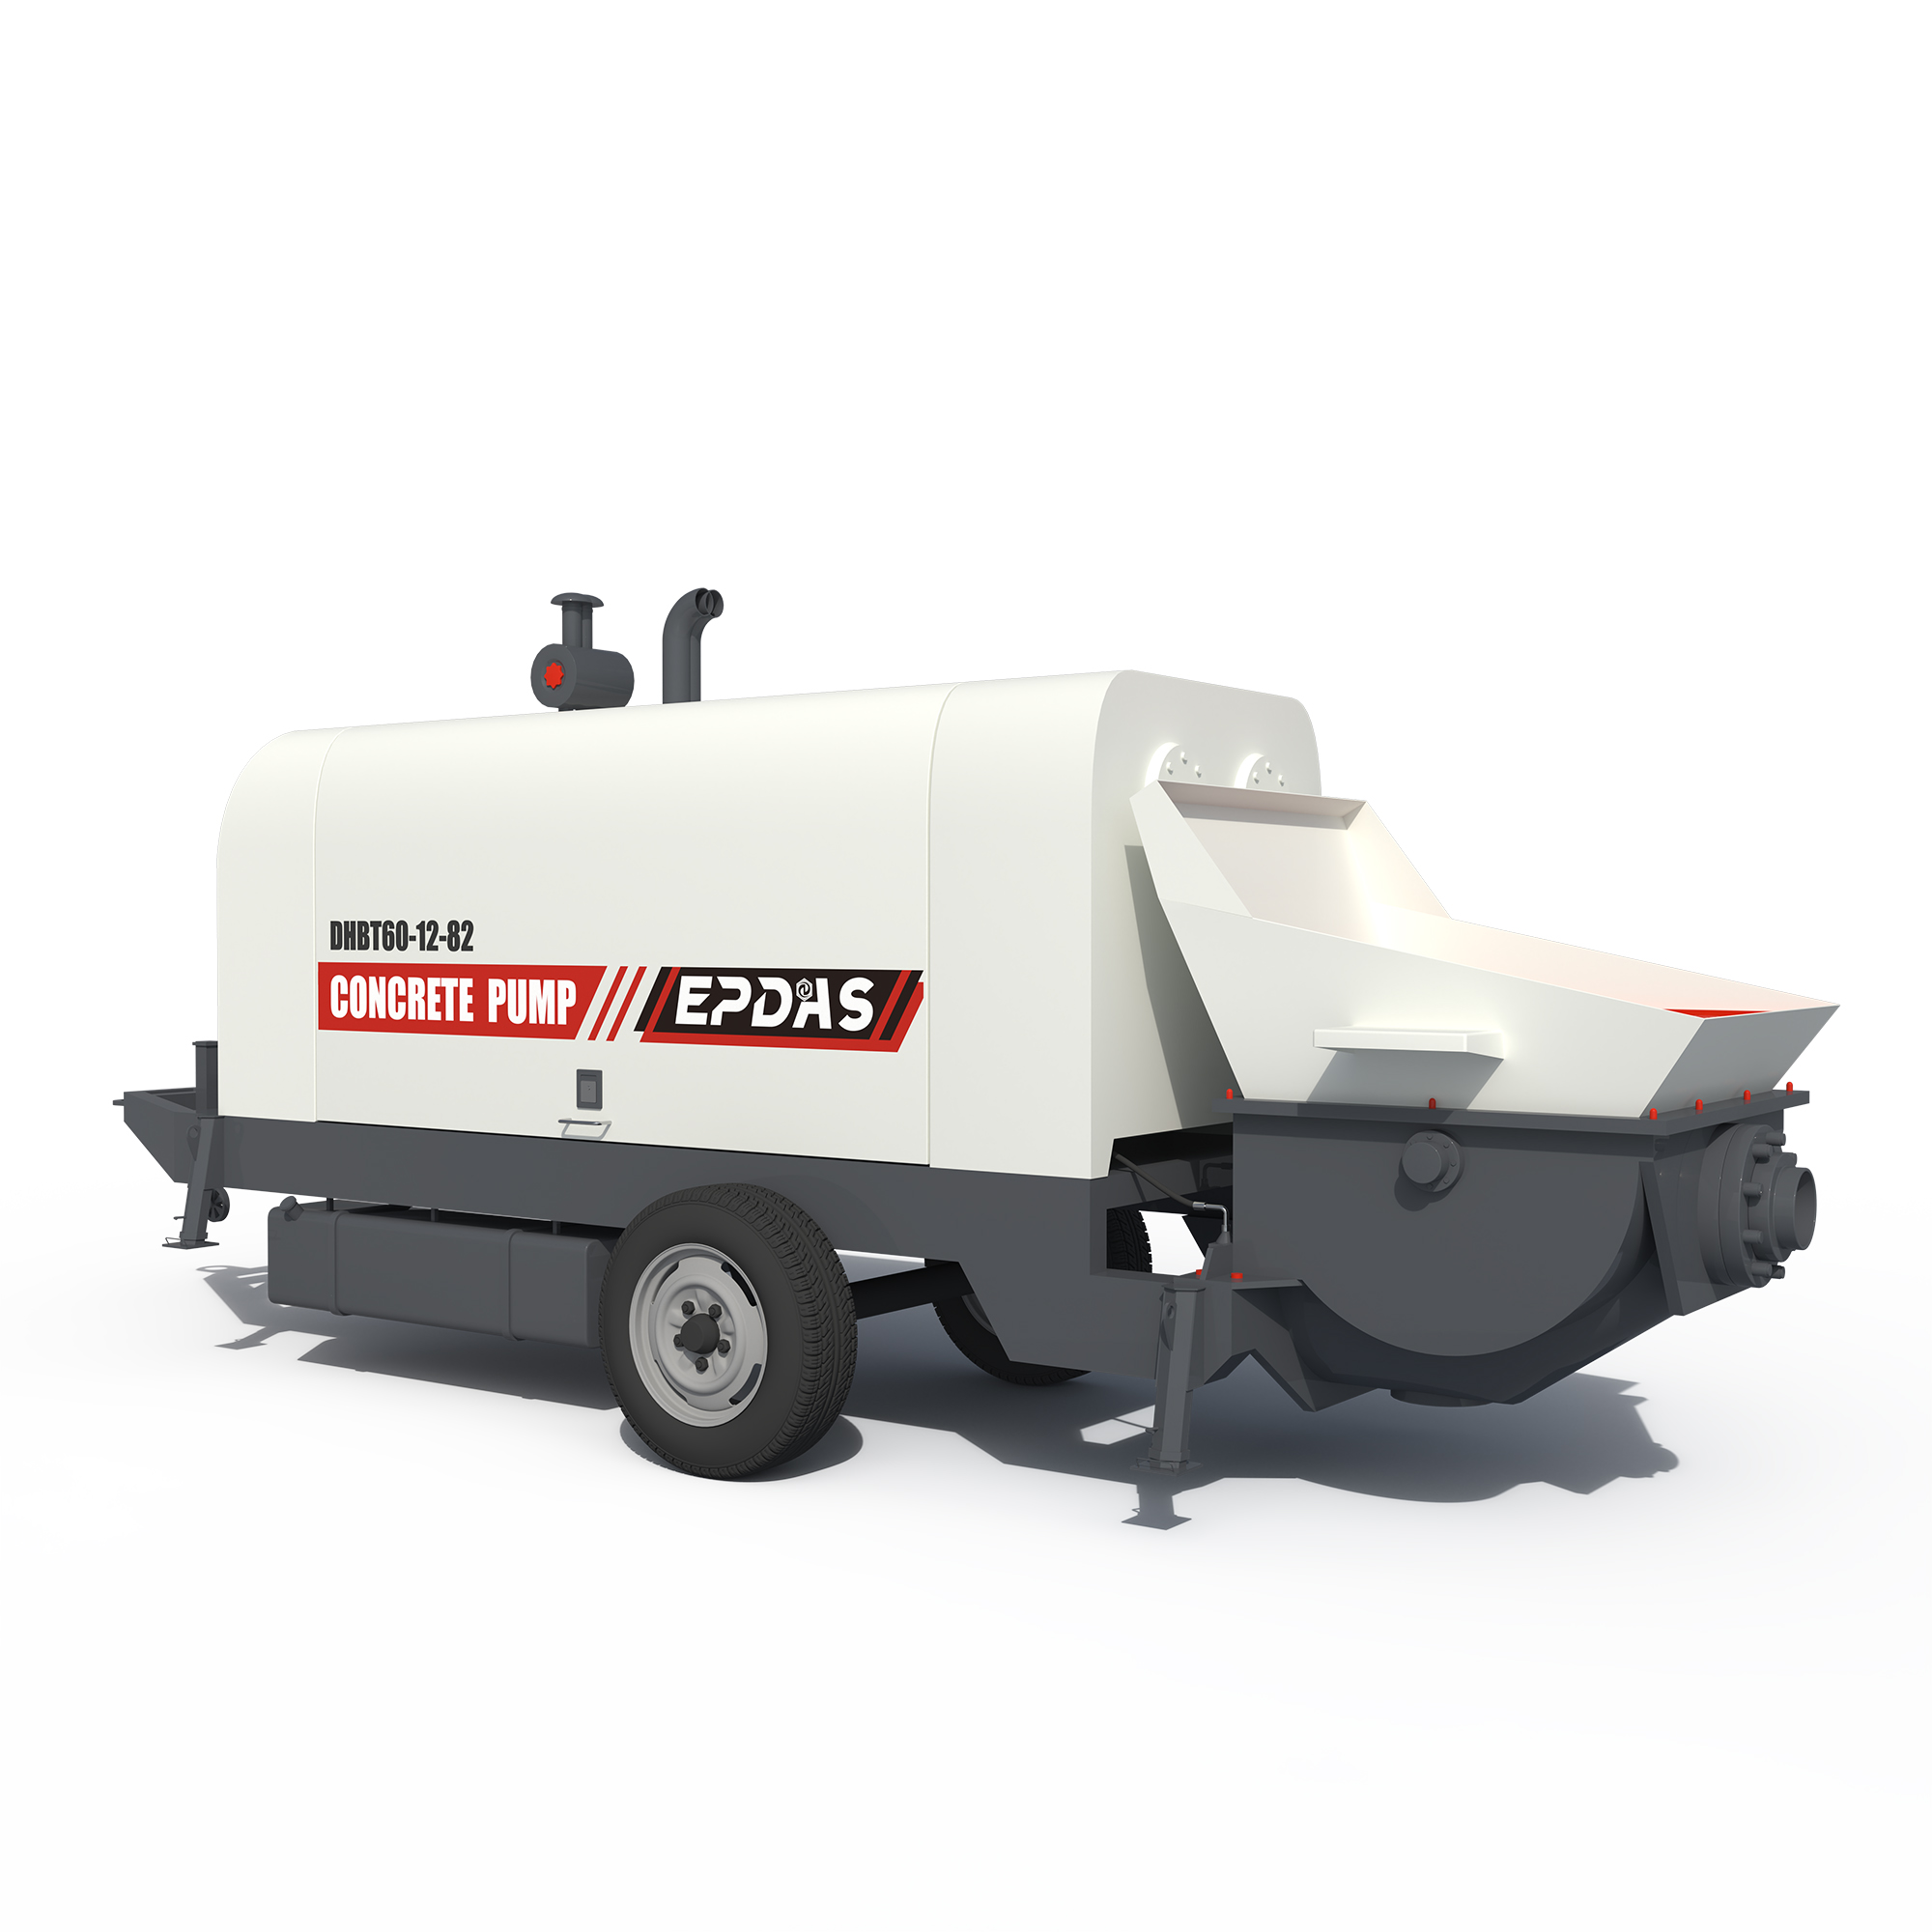 INTERFACE 03 / Trailer Concrete Pump
Concrete produced by HZS120 can be delivered to a separately positioned pumping operation.
Define whether a truck or another engineered transfer arrangement supplies the pump and how arrivals are scheduled.
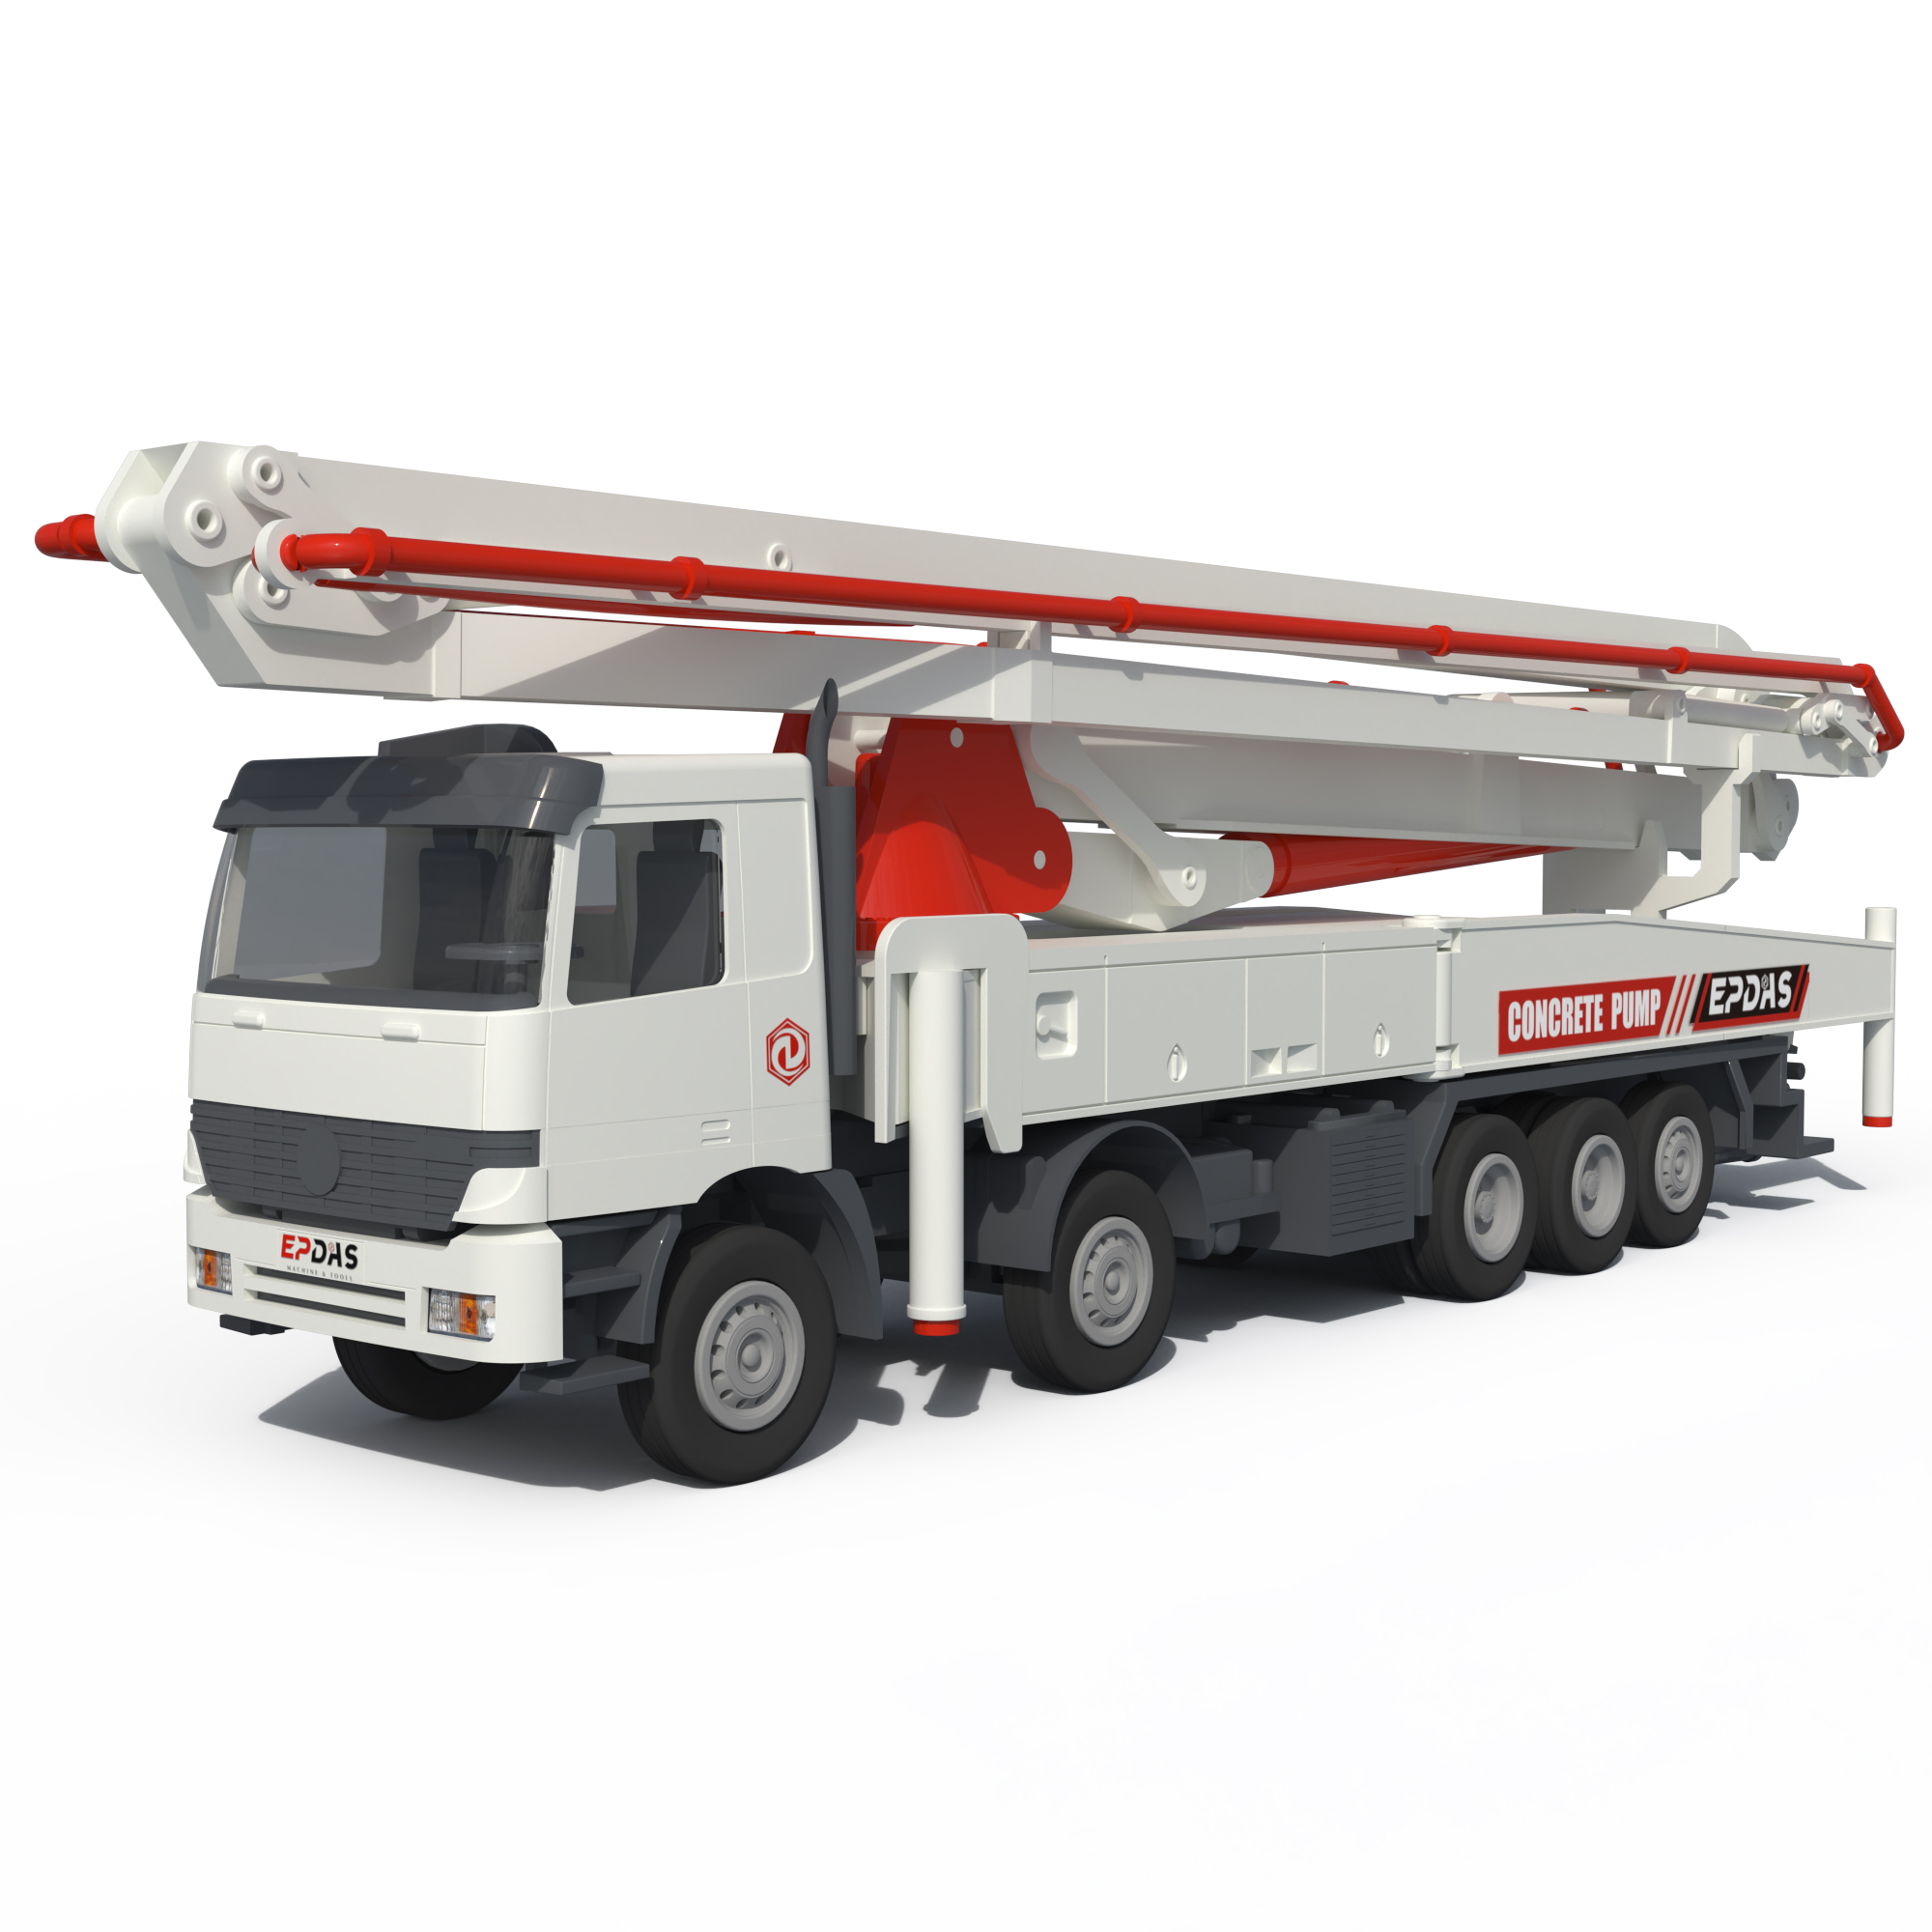 INTERFACE 04 / Concrete Boom Pump
A truck-mounted pump provides distribution at the pour after the plant has prepared the mix.
Match delivery access and concrete consistency to the selected pump, without treating the 120 m³/h plant reference as its guaranteed supply.
Options and alternative architectures are identified in each explanation. This is not a pre-approved matched package. Final connections, duty and supplied components require a model-specific technical review.
Review My Equipment CombinationSeparate the key systems to see what each contributes to the operation.
HZS120 functional separation illustration. Blocks identify subsystem roles; they do not reproduce the machine geometry, assembly sequence or fastening details. Request the approved model drawing for engineering use.
| Parameter | HZS120 |
|---|---|
| Theoretical productivity (m3/hr) | 120 |
| Mixer model | JS2000 |
| Mixing motor power (kw) | 2*37 |
| Feeding mode | Belt conveyor |
| Cycling period (s) | 60 |
| Max. aggregate size (mm) | Ф80 |
| Aggregate bins capacity (m3) | 4*20 |
| Discharging height (m) | 4.0 |
| Aggregate weighing precision | ±2% |
| Powder weighing precision | ±1% |
| Water weighing precision | ±1% |
| Additive weighing precision | ±1% |
Published EPDAS specifications are a reference for equipment selection. Final specifications and included equipment are confirmed in the quotation.
Original EPDAS Technical Reference ↗| Selection reference | HZS120 · This model | HZS90 | HZS150 |
|---|---|---|---|
| Theoretical productivity (m3/hr) | 120 | 90 | 150 |
| Mixer model | JS2000 | JS1500 | JS3000 |
| Mixing motor power (kw) | 2*37 | 55 | 2*55 |
| Aggregate bins capacity (m3) | 4*20 | 3*12 | 4*20 |
| Discharging height (m) | 4.0 | 4.0 | 4.0 |
Consider HZS120 for a ready-mix or construction supply operation planning around four aggregate materials and regular demand.
Four aggregate materials and the recipe proportions for the proposed production schedule.
JS2000 utility requirements, mixer access and the selected control arrangement.
Truck entry, 4.0 m discharge clearance and loading-to-departure circulation.
Confirm core equipment, options, buyer-provided systems, transport modules, inspection documents and support responsibilities in the quotation.