HZS90 Configuration
The mixer drive rises to 55 kW to match the larger mixing unit.
HZS90 increases the belt-fed plant rating to 90 m³/h through a JS1500 mixer. Its three 12 m³ aggregate compartments retain the same published storage format as HZS60.
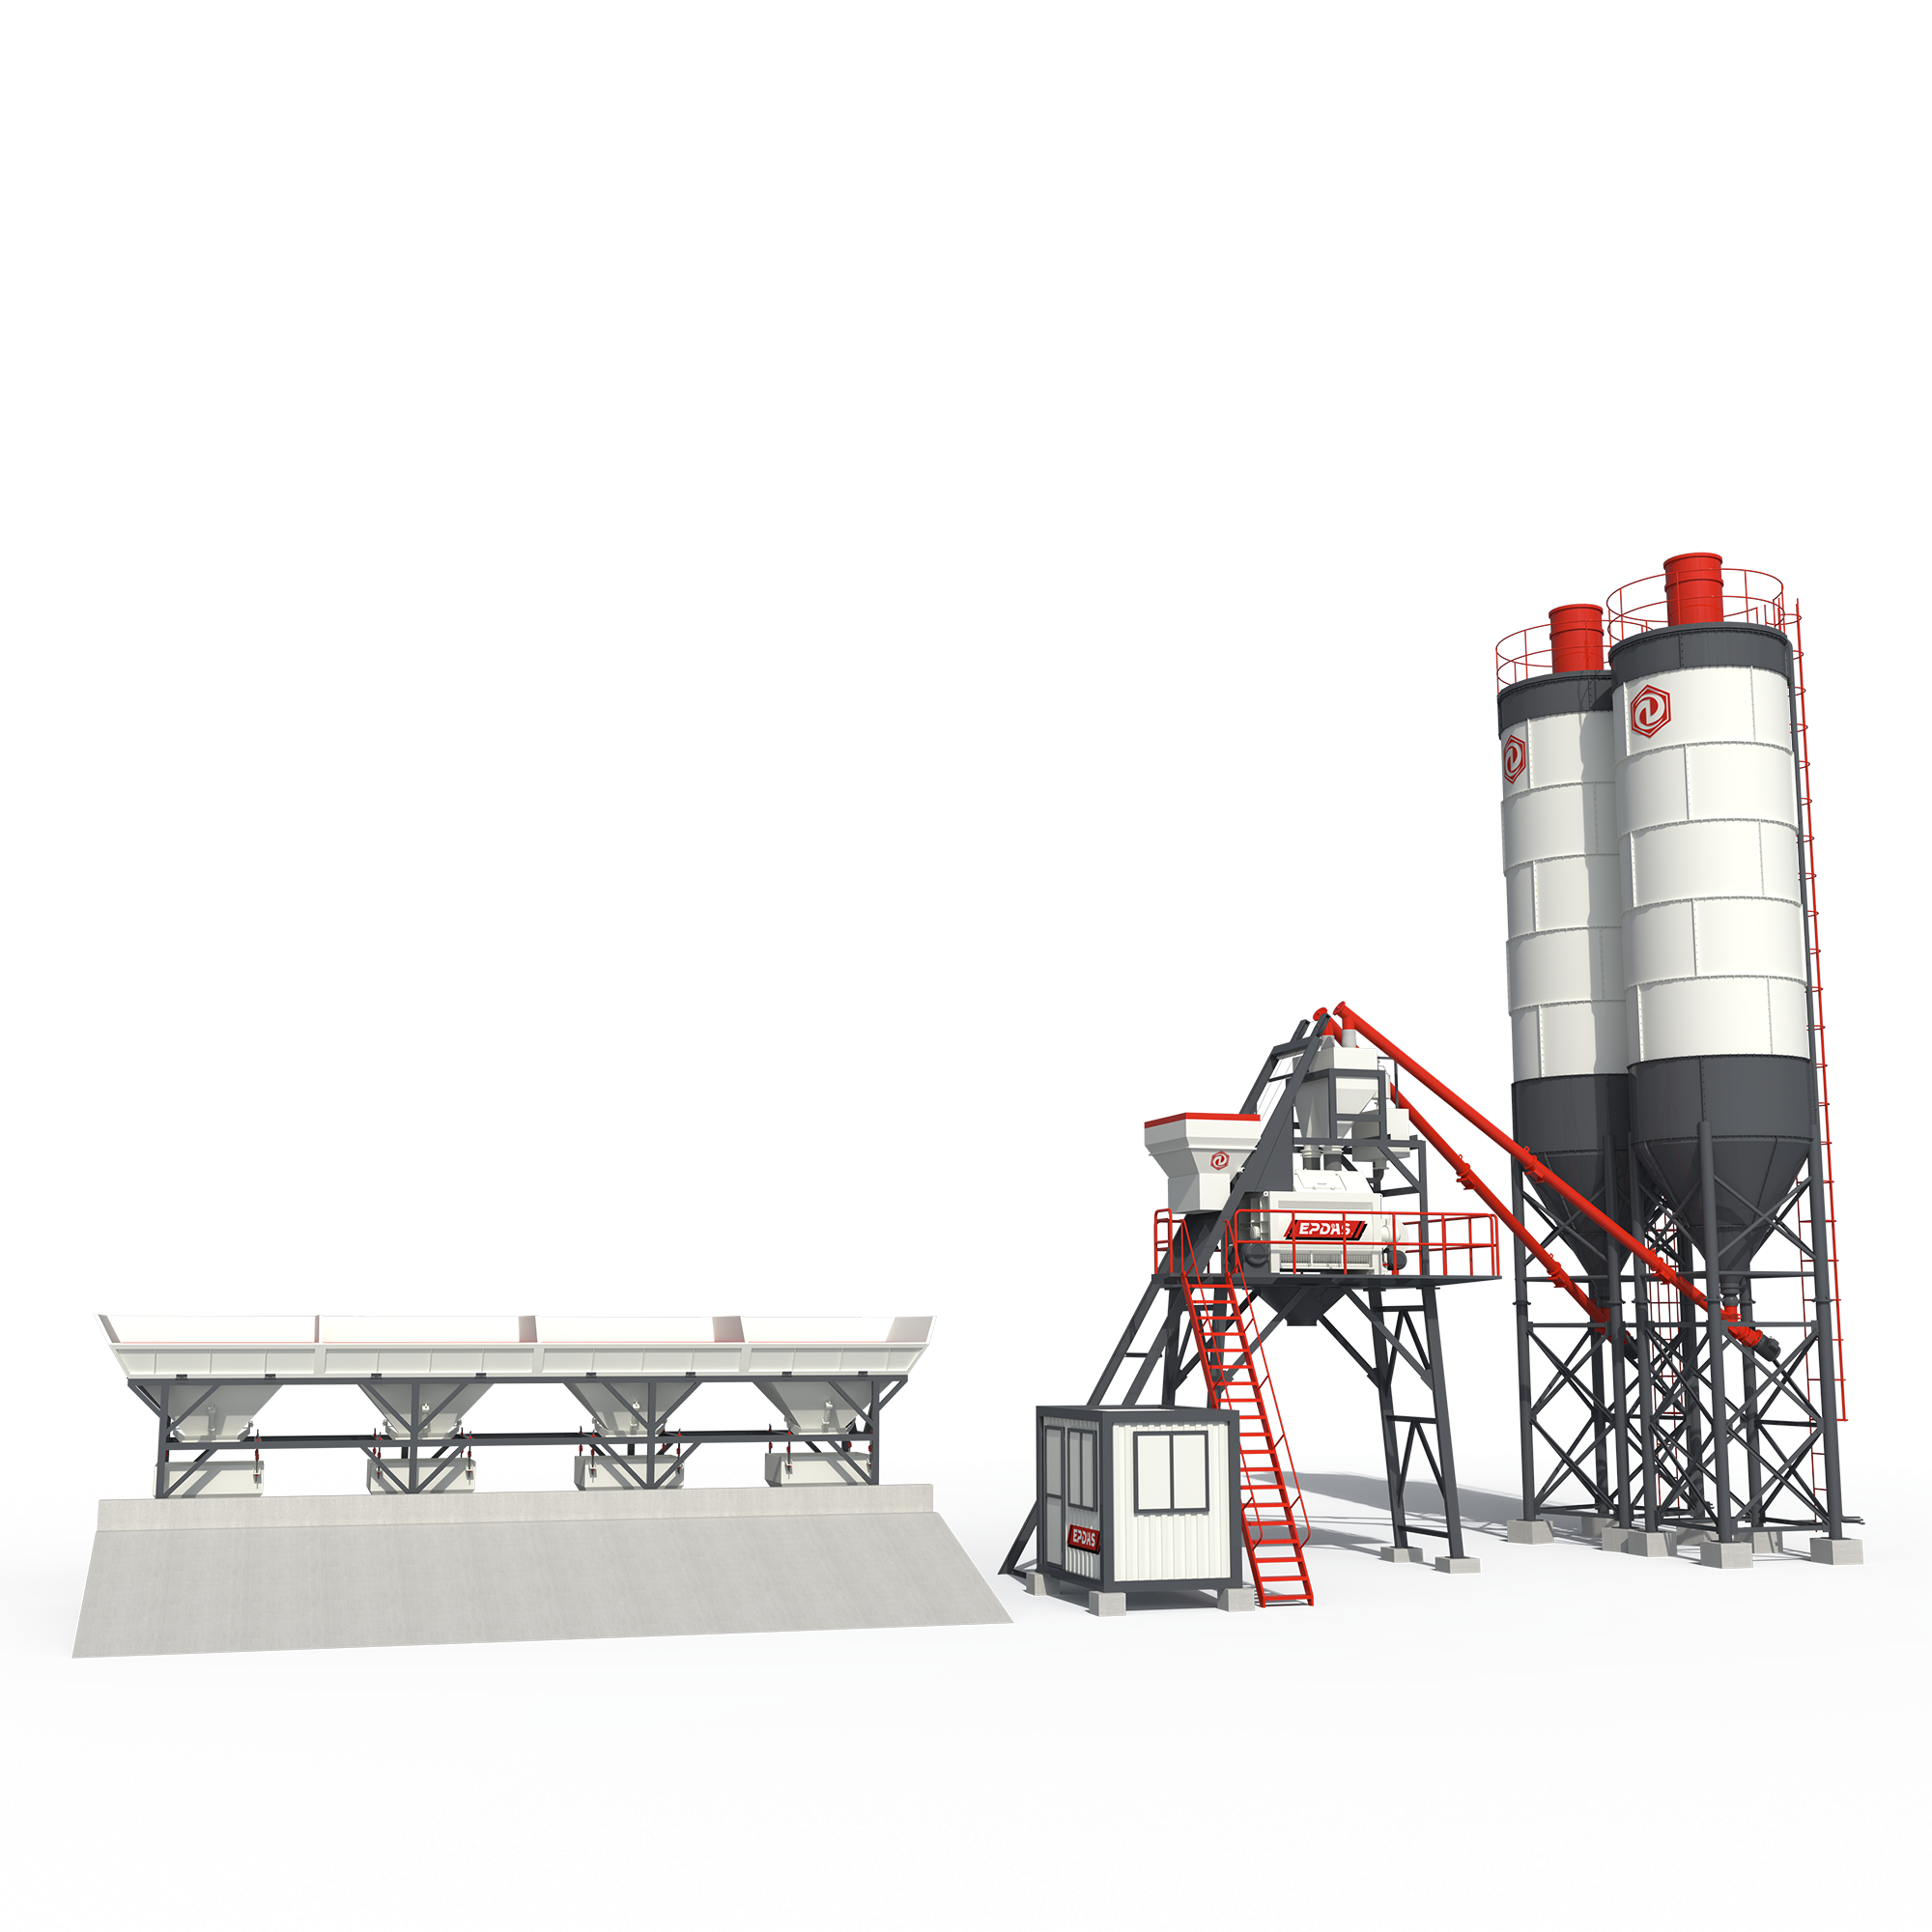
Series rendering. Confirm HZS90's appearance and included equipment in its proposal.
This model increases the mixer class while retaining the published three 12 m³ aggregate compartments of the smaller belt-fed configuration.
Assess it when the production plan needs the JS1500 stage but does not require four independently stored fractions.
The mixer drive rises to 55 kW to match the larger mixing unit.
Keeping the three-bin format can suit a concrete mix plan that does not require a fourth aggregate compartment.
Understand the role of each connection before building the equipment package.
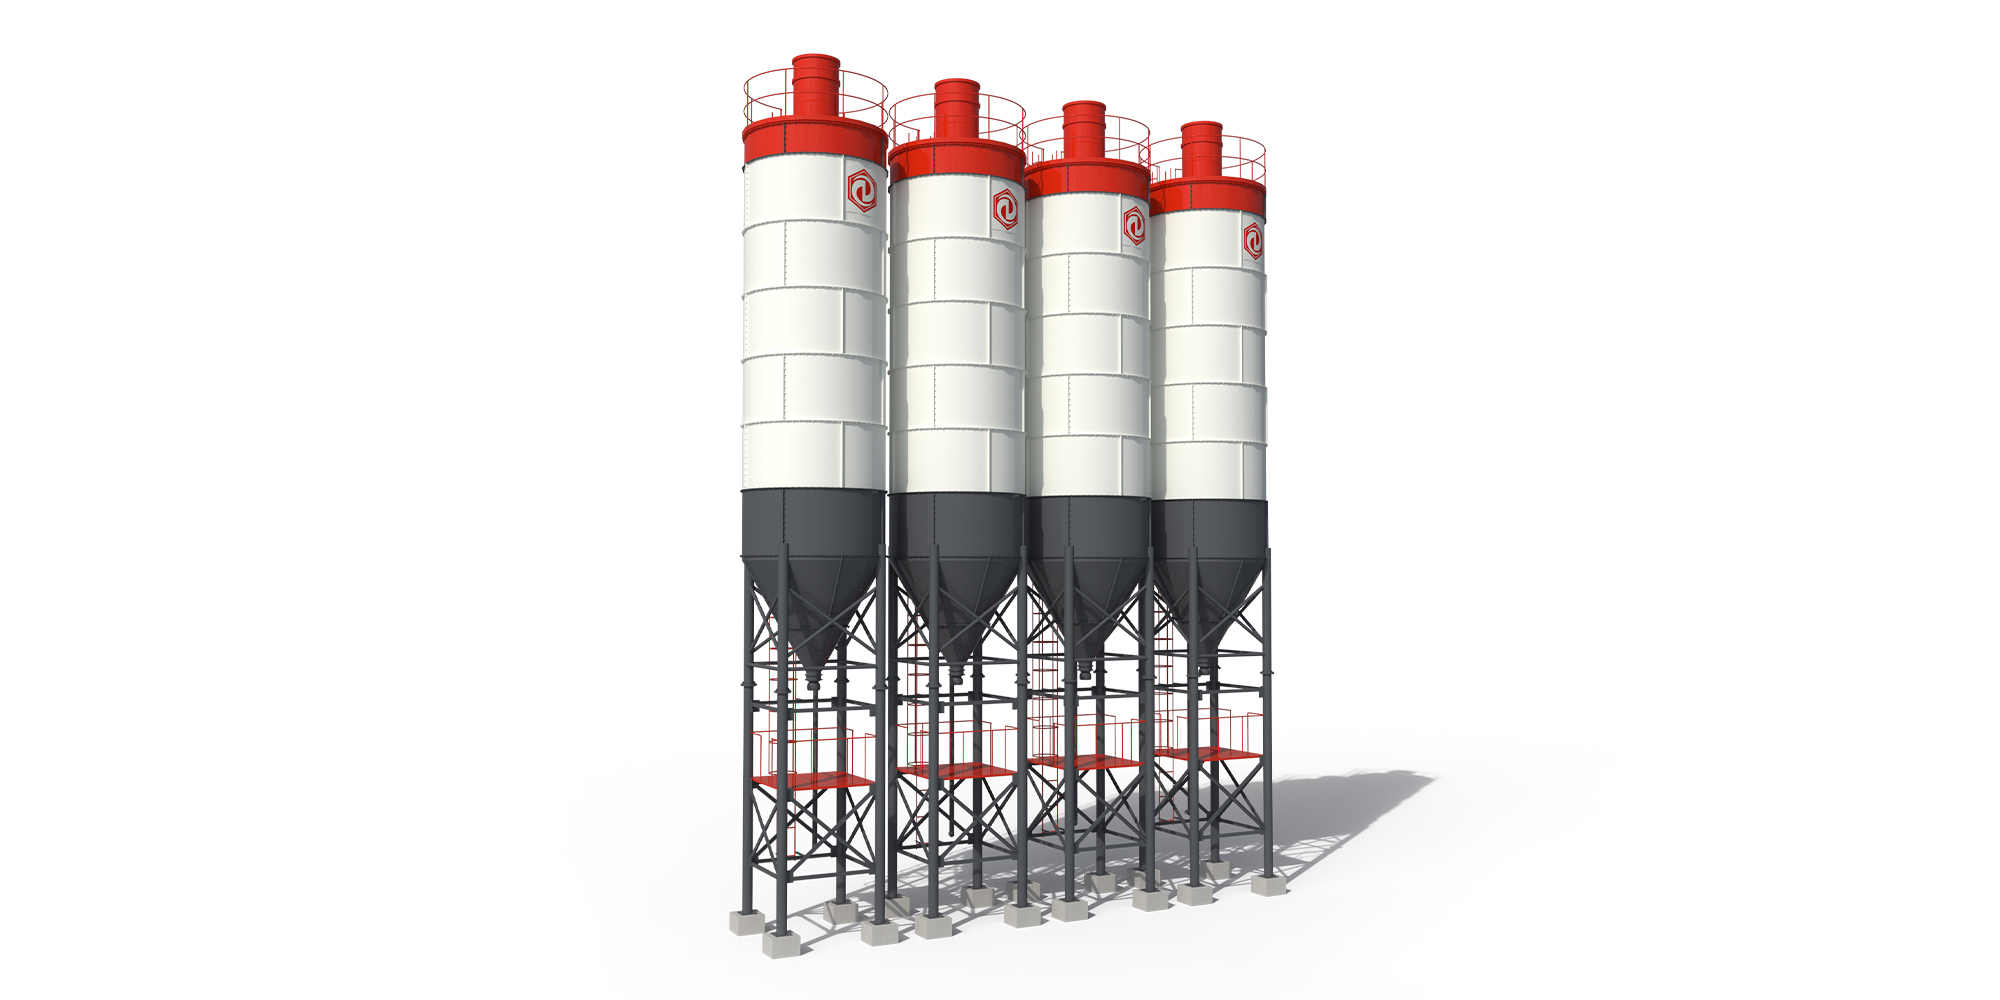 INTERFACE 01 / Cement Silo
Cement stock must follow the higher mixing demand.
Retain space for replenishment without obstructing the three aggregate loading areas.
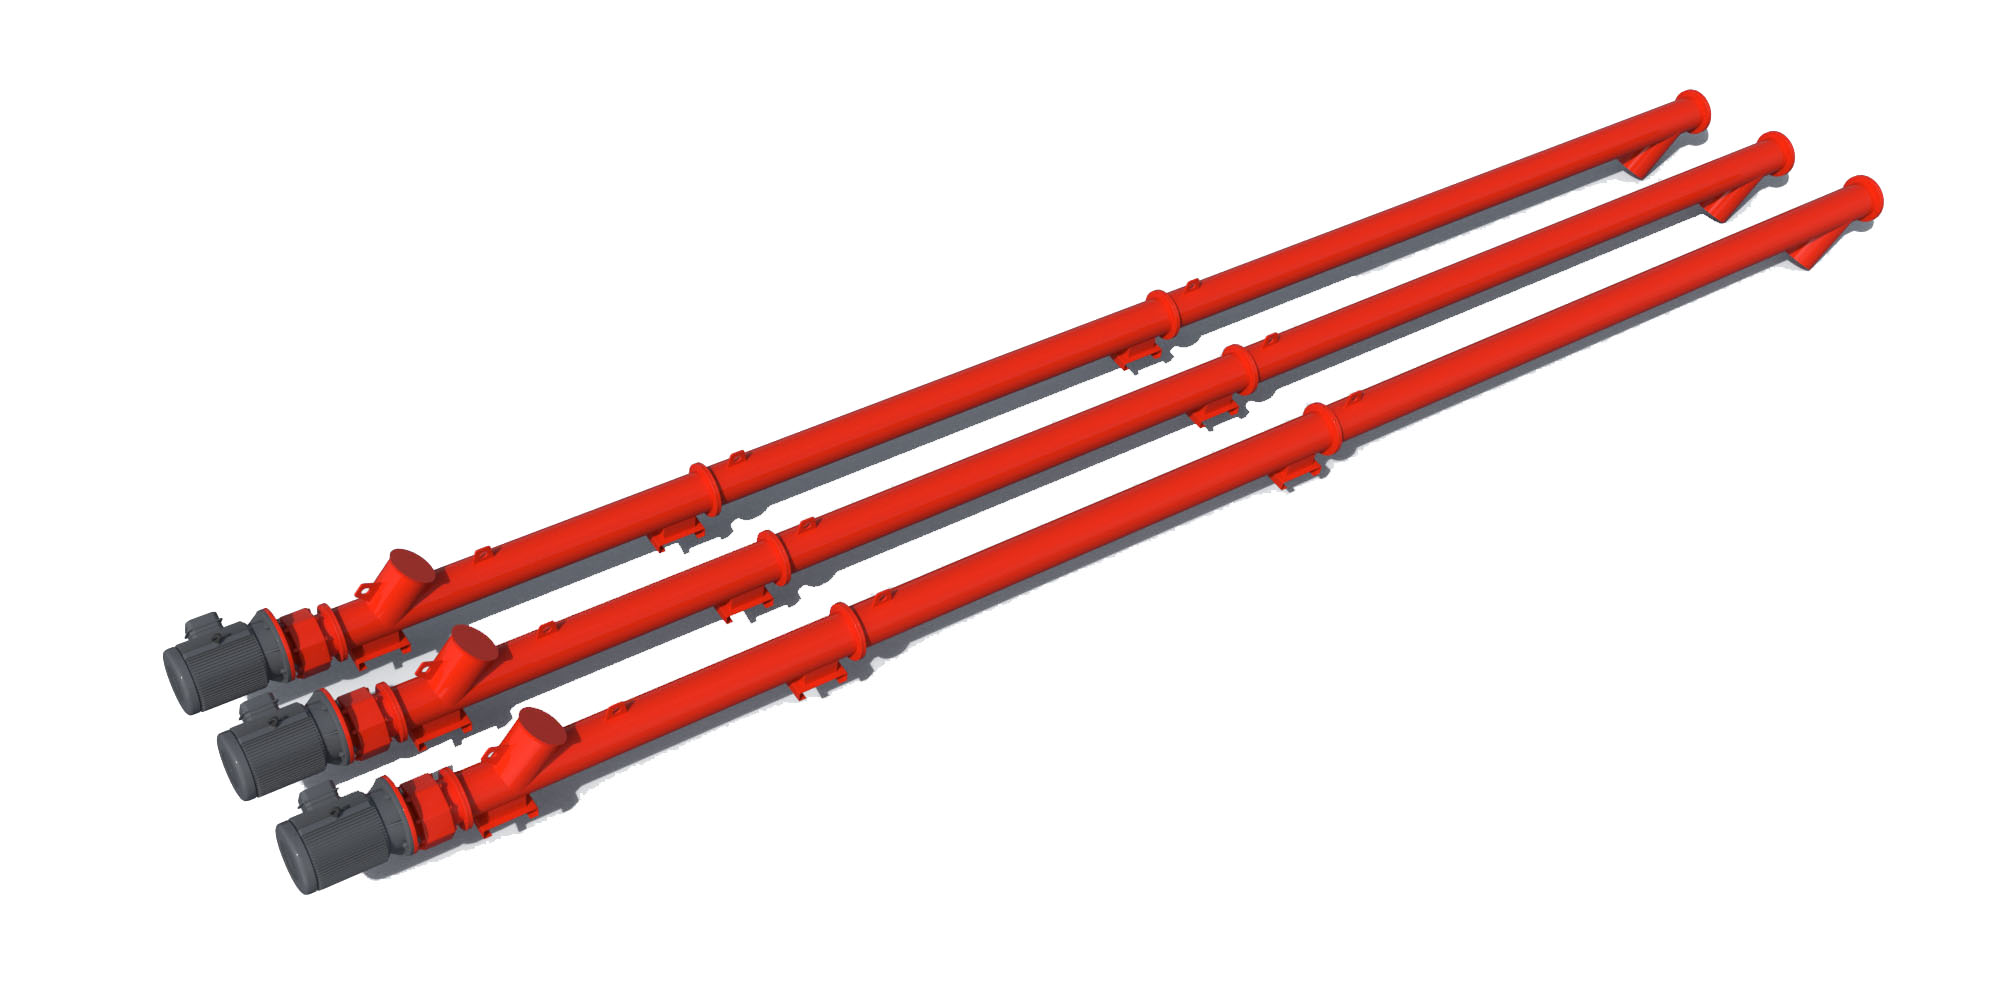 INTERFACE 02 / Screw Conveyor
The feed system needs a duty review as mixer class increases.
Identical site geometry does not establish sufficient powder capacity.
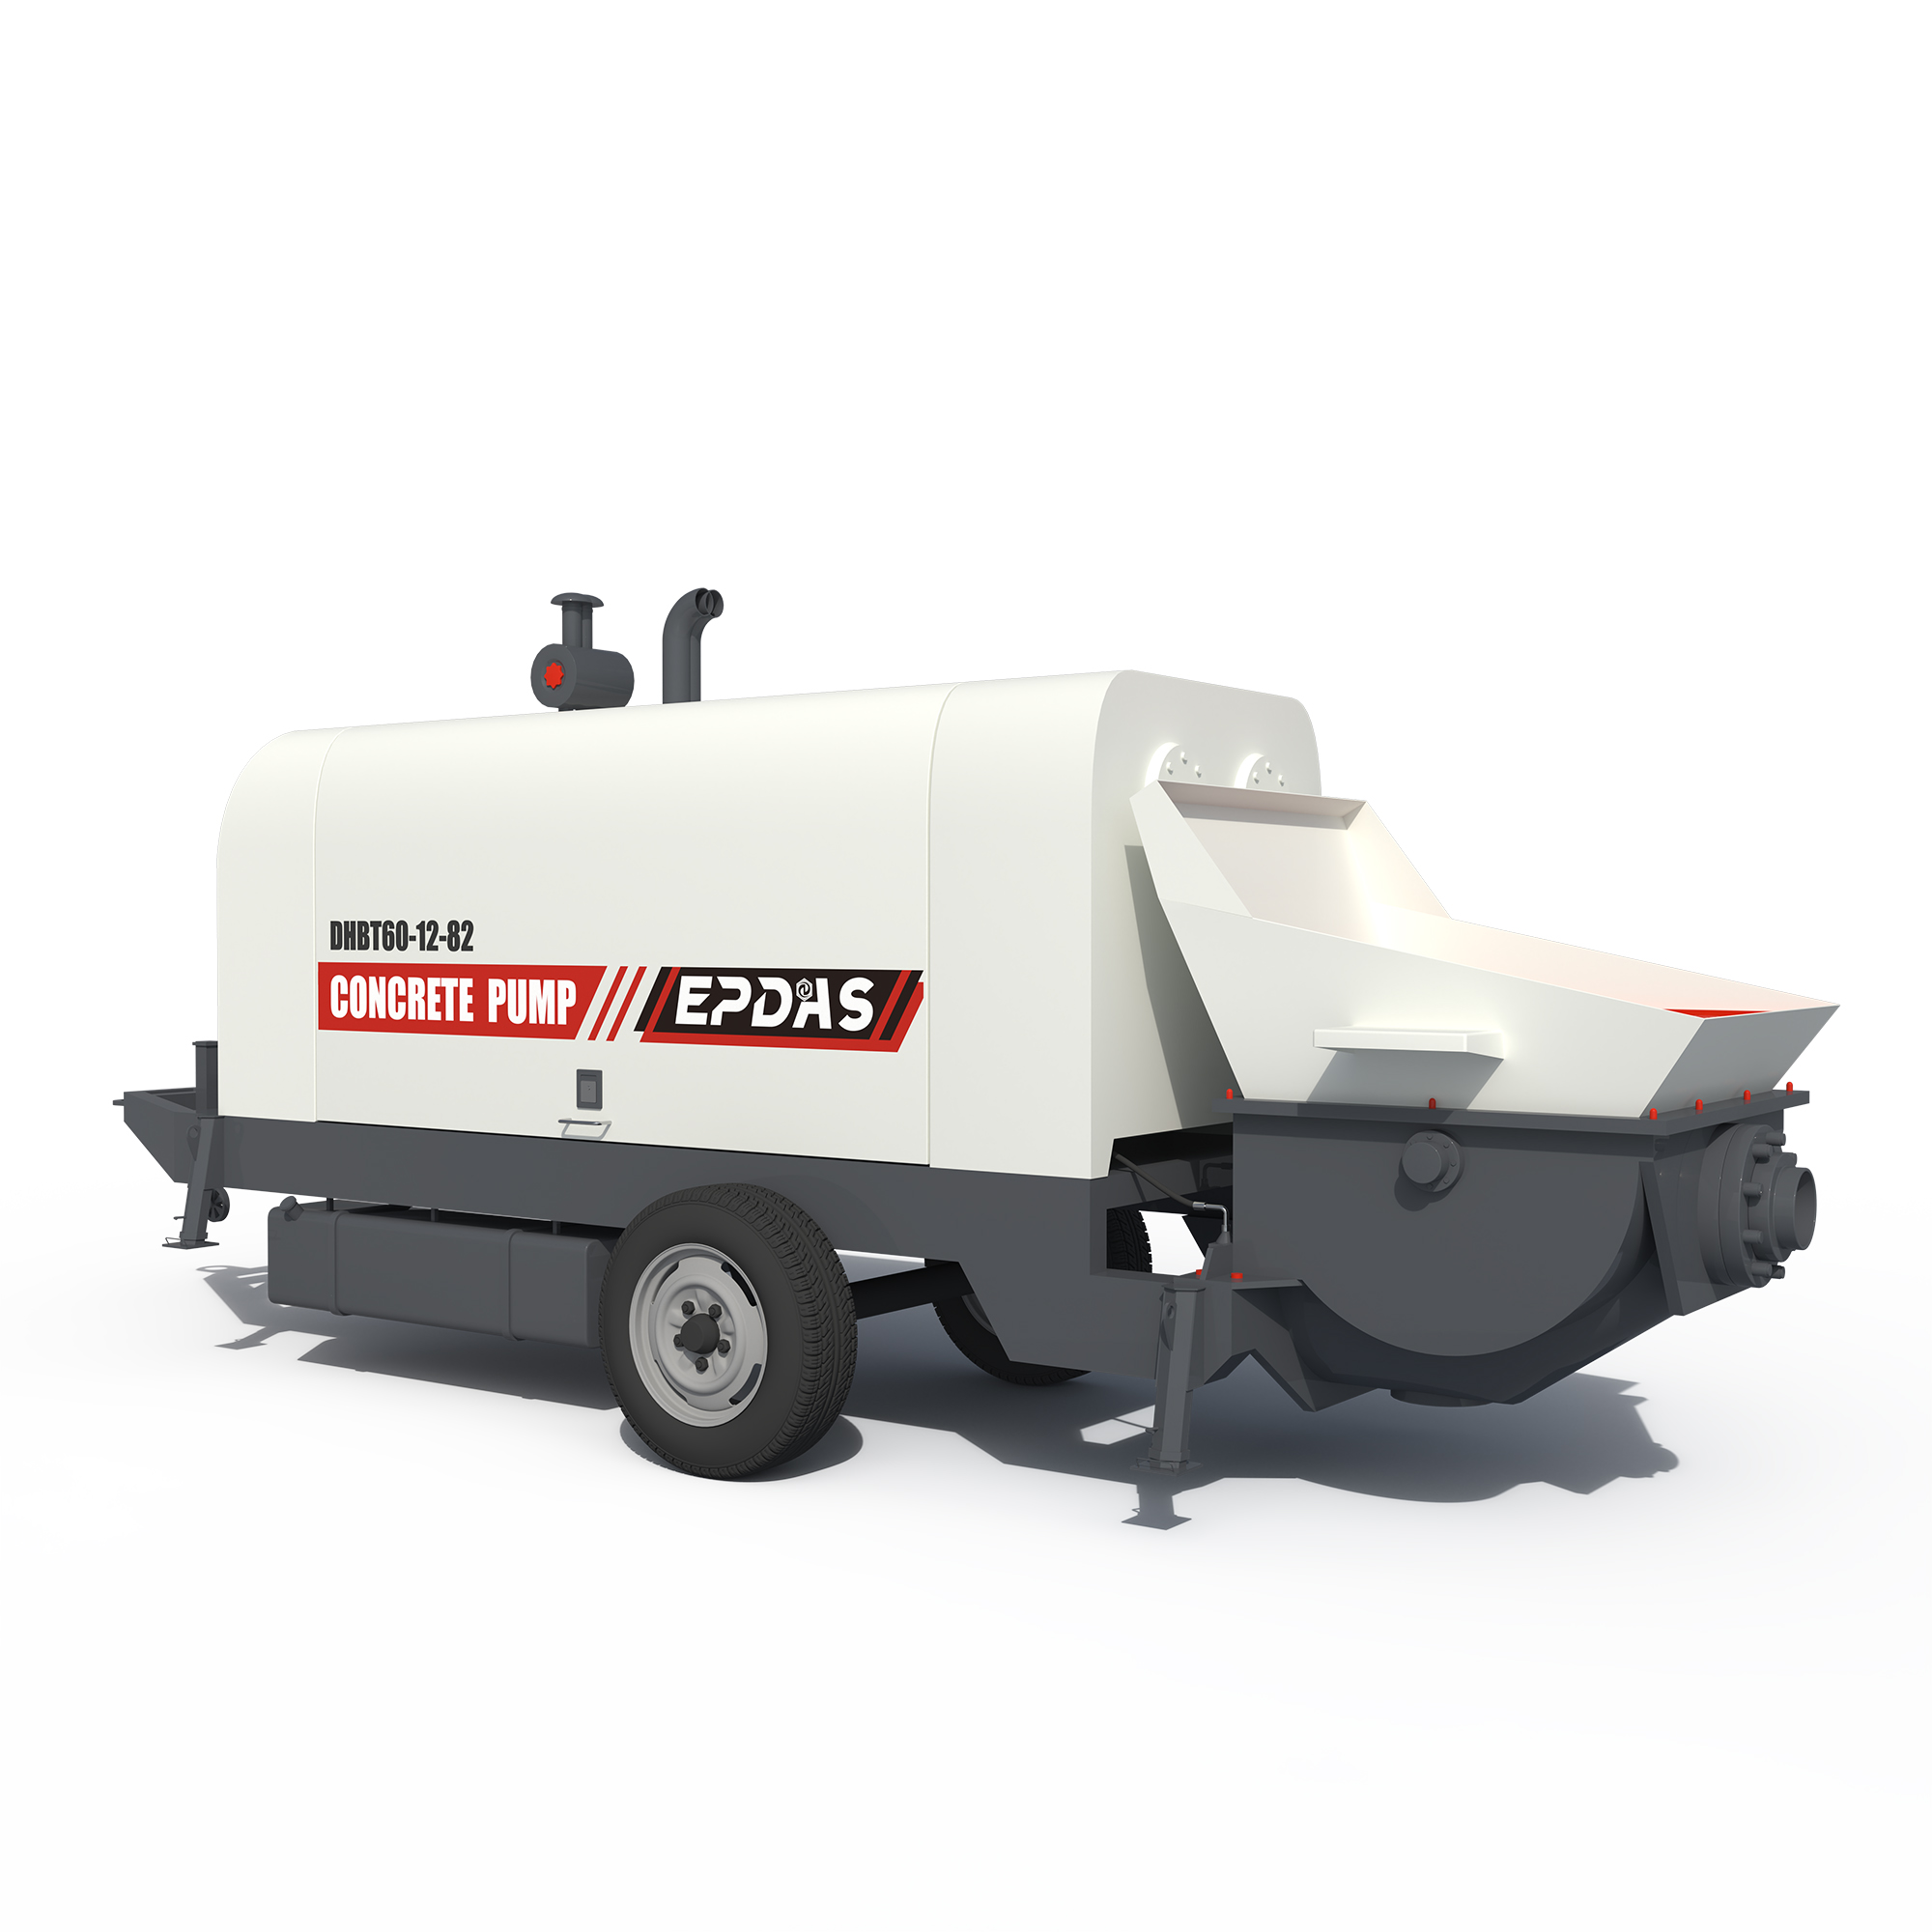 INTERFACE 03 / Trailer Concrete Pump
A pump can distribute concrete from the production operation.
Establish truck turnaround and receiving rhythm for the intended pours.
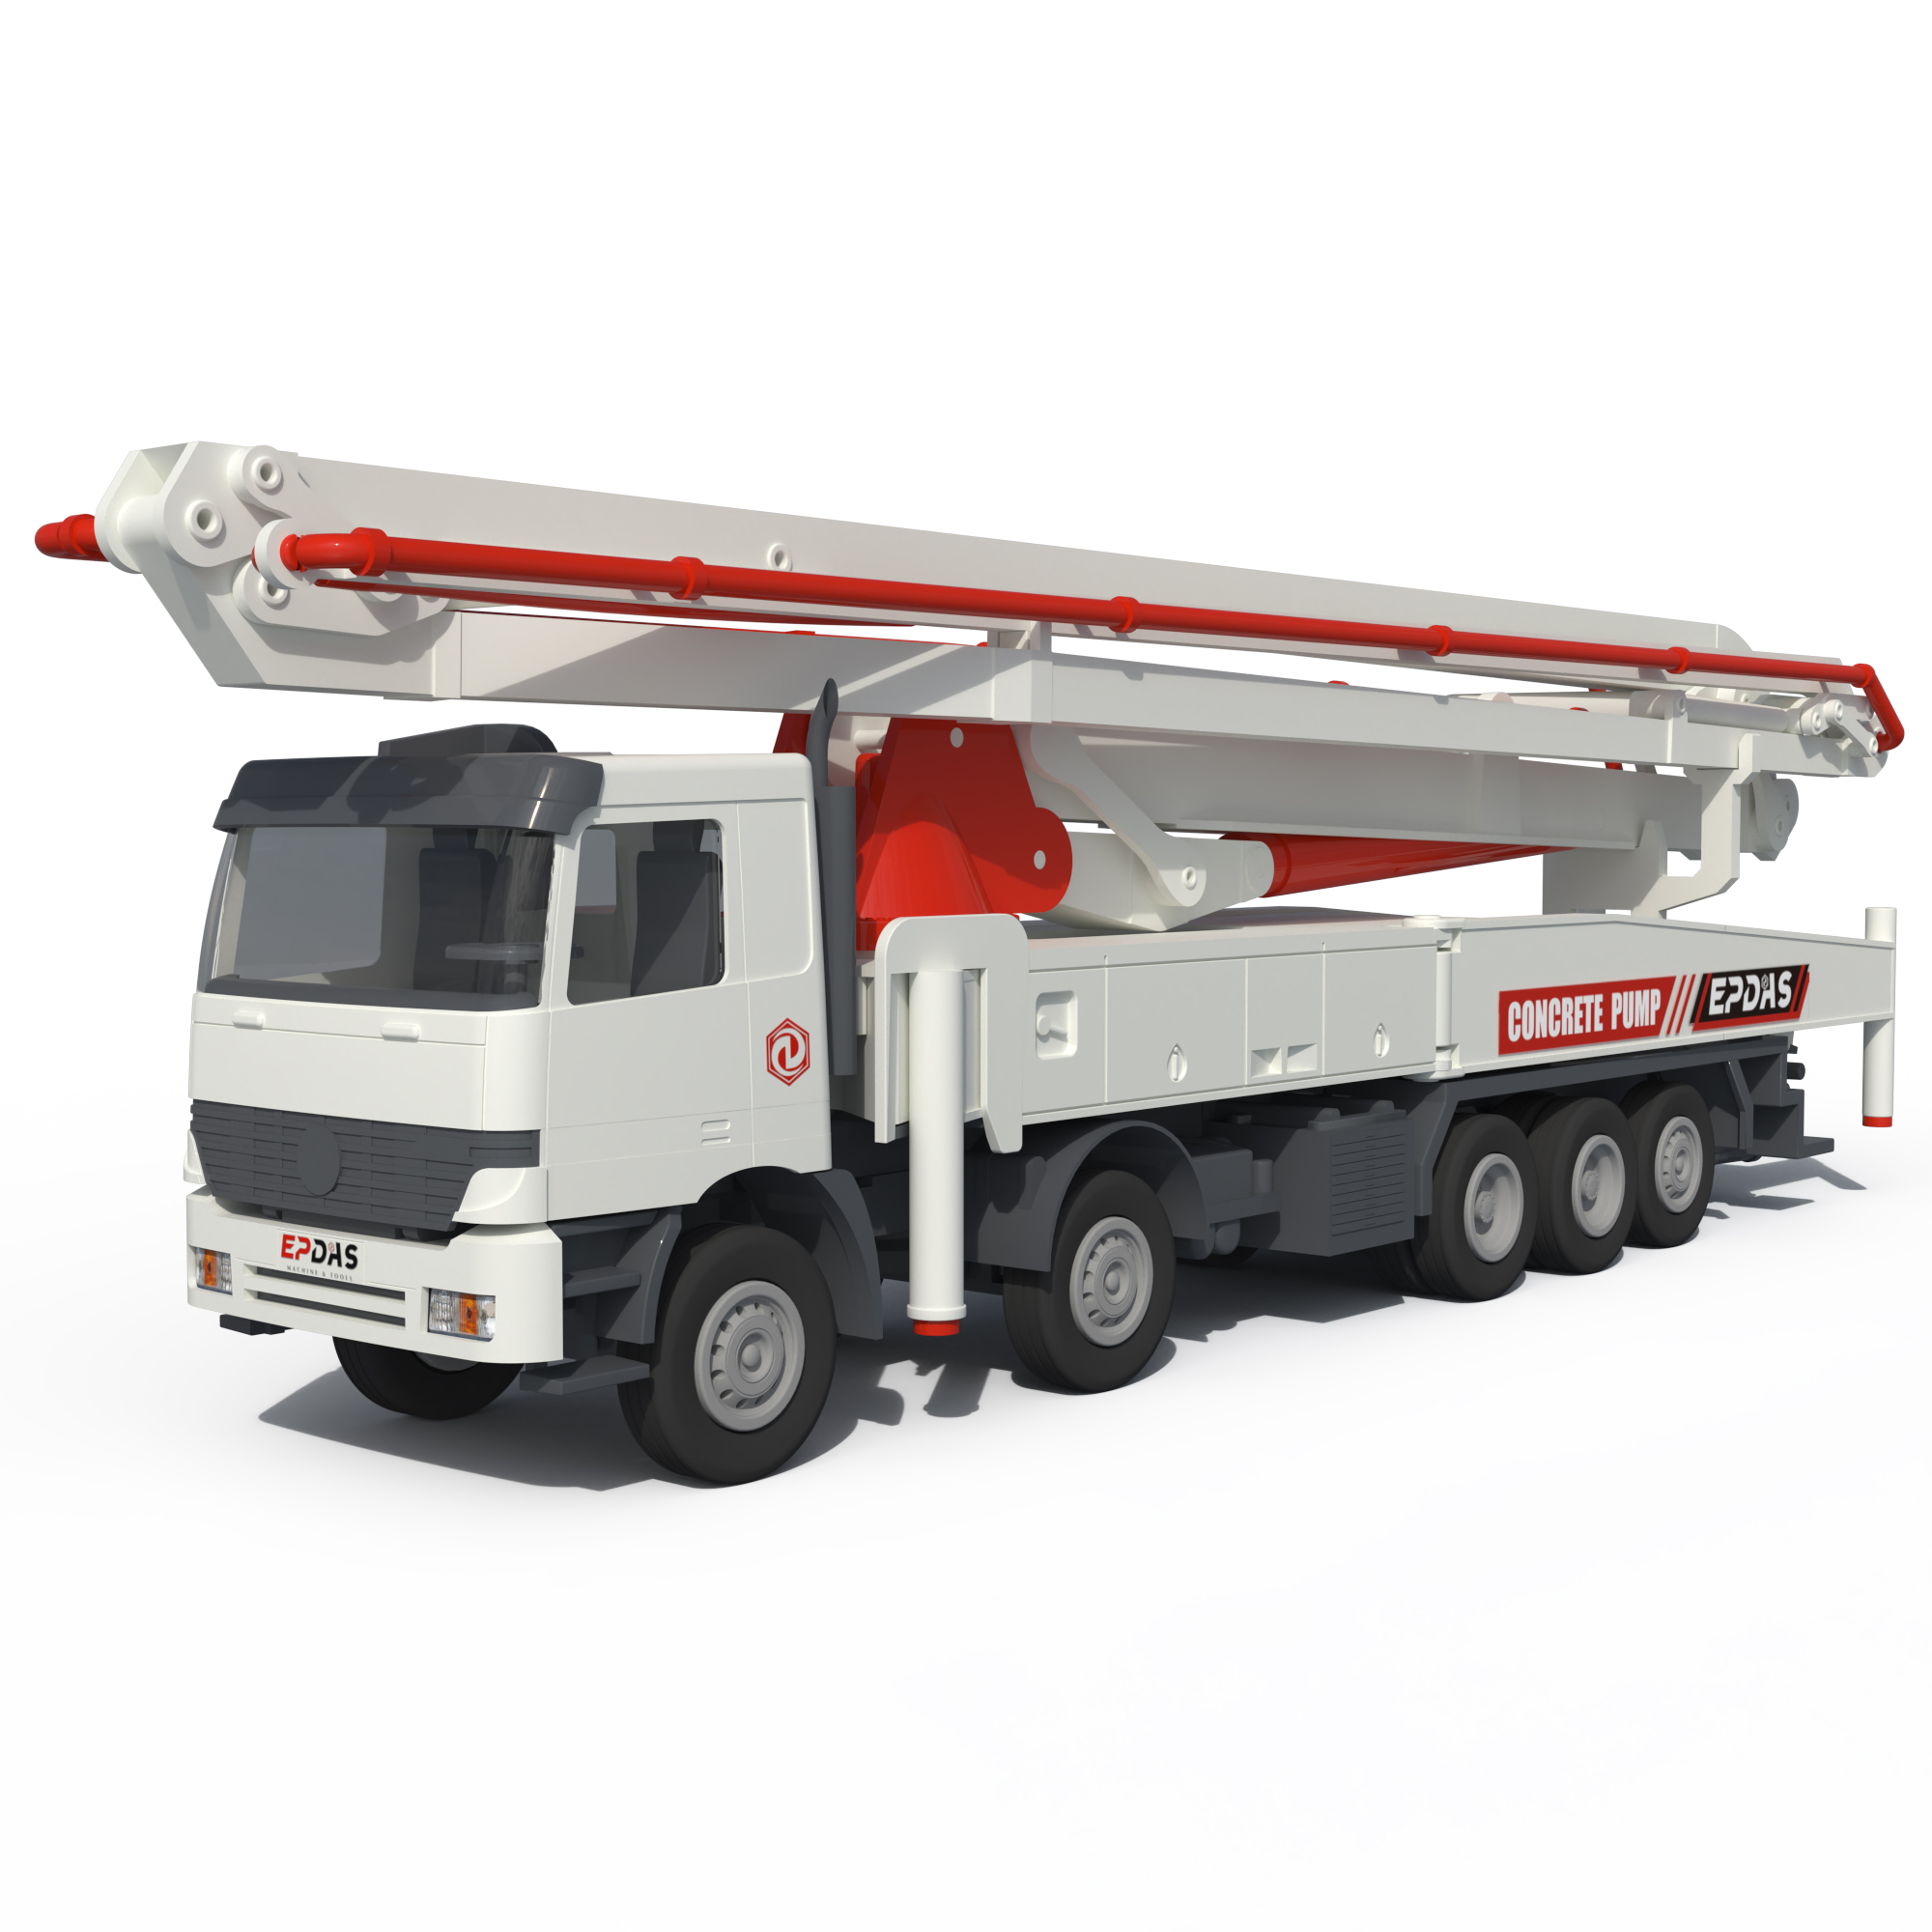 INTERFACE 04 / Concrete Boom Pump
Mobile placing at a destination needs consistent mixed-concrete deliveries.
Coordinate dispatch separately from the 90 m³/h theoretical value.
Options and alternative architectures are identified in each explanation. This is not a pre-approved matched package. Final connections, duty and supplied components require a model-specific technical review.
Review My Equipment CombinationSeparate the key systems to see what each contributes to the operation.
HZS90 functional separation illustration. Blocks identify subsystem roles; they do not reproduce the machine geometry, assembly sequence or fastening details. Request the approved model drawing for engineering use.
| Parameter | HZS90 |
|---|---|
| Theoretical productivity (m3/hr) | 90 |
| Mixer model | JS1500 |
| Mixing motor power (kw) | 55 |
| Feeding mode | Belt conveyor |
| Cycling period (s) | 60 |
| Max. aggregate size (mm) | Ф80 |
| Aggregate bins capacity (m3) | 3*12 |
| Discharging height (m) | 4.0 |
| Aggregate weighing precision | ±2% |
| Powder weighing precision | ±1% |
| Water weighing precision | ±1% |
| Additive weighing precision | ±1% |
Published EPDAS specifications are a reference for equipment selection. Final specifications and included equipment are confirmed in the quotation.
Original EPDAS Technical Reference ↗| Selection reference | HZS90 · This model | HZS60 | HZS120 |
|---|---|---|---|
| Theoretical productivity (m3/hr) | 90 | 60 | 120 |
| Mixer model | JS1500 | JS1000 | JS2000 |
| Feeding mode | Belt conveyor | Belt conveyor | Belt conveyor |
| Aggregate bins capacity (m3) | 3*12 | 3*12 | 4*20 |
| Discharging height (m) | 4.0 | 4.0 | 4.0 |
Assess this model when mixer output needs to increase without selecting the four-bin HZS120 arrangement.
Mixer model: JS1500
Mixing motor power (kw): 55
Aggregate bins capacity (m3): 3*12
Confirm core equipment, options, buyer-provided systems, transport modules, inspection documents and support responsibilities in the quotation.