HZS60 Configuration
The belt conveyor changes the aggregate delivery arrangement from the hopper-fed HZS50 alternative.
HZS60 combines belt aggregate feeding with a JS1000 mixer and a 60 m³/h theoretical rating. It is the smallest belt-fed option in the published stationary range.
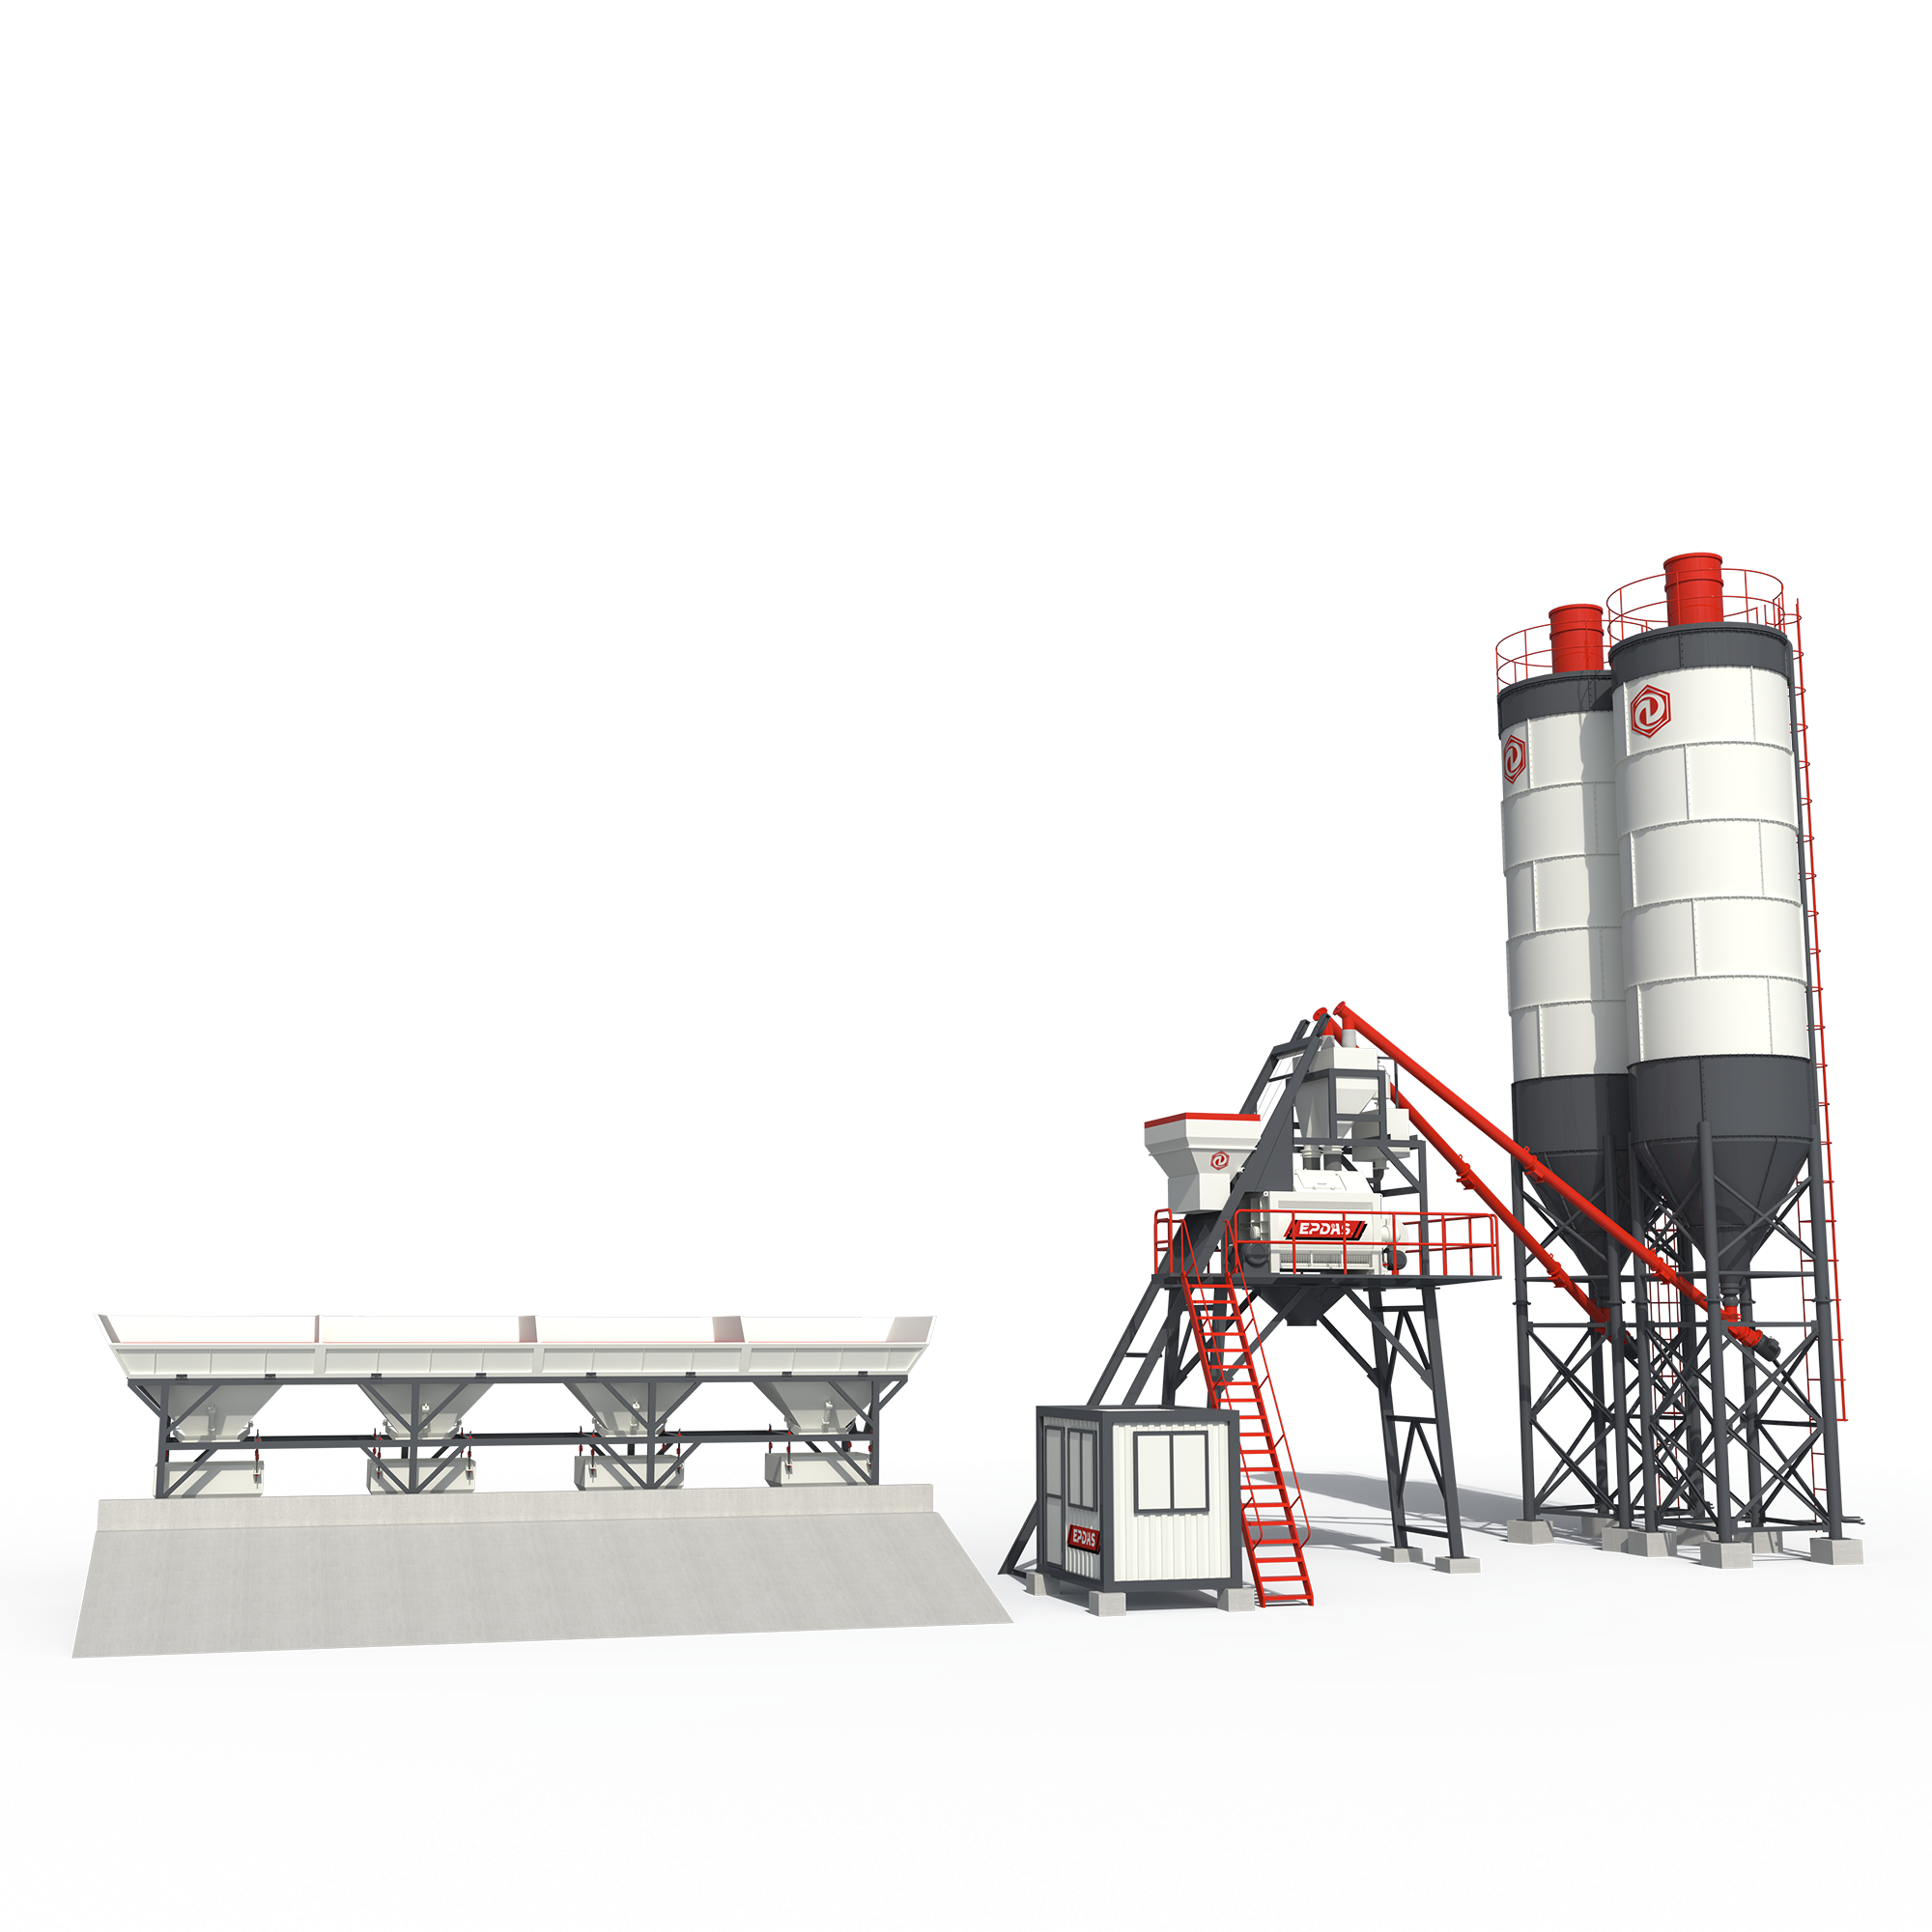
Series rendering. Confirm HZS60's appearance and included equipment in its proposal.
Belt feeding supplies the JS1000 central mixer in the smallest conveyor-fed model of the current stationary table.
Use this configuration to study a permanent production yard organised around conveyor access rather than a hoist bucket.
The belt conveyor changes the aggregate delivery arrangement from the hopper-fed HZS50 alternative.
A listed 60-second cycle and three 12 m³ aggregate bins provide clear starting values for a production-layout discussion.
Understand the role of each connection before building the equipment package.
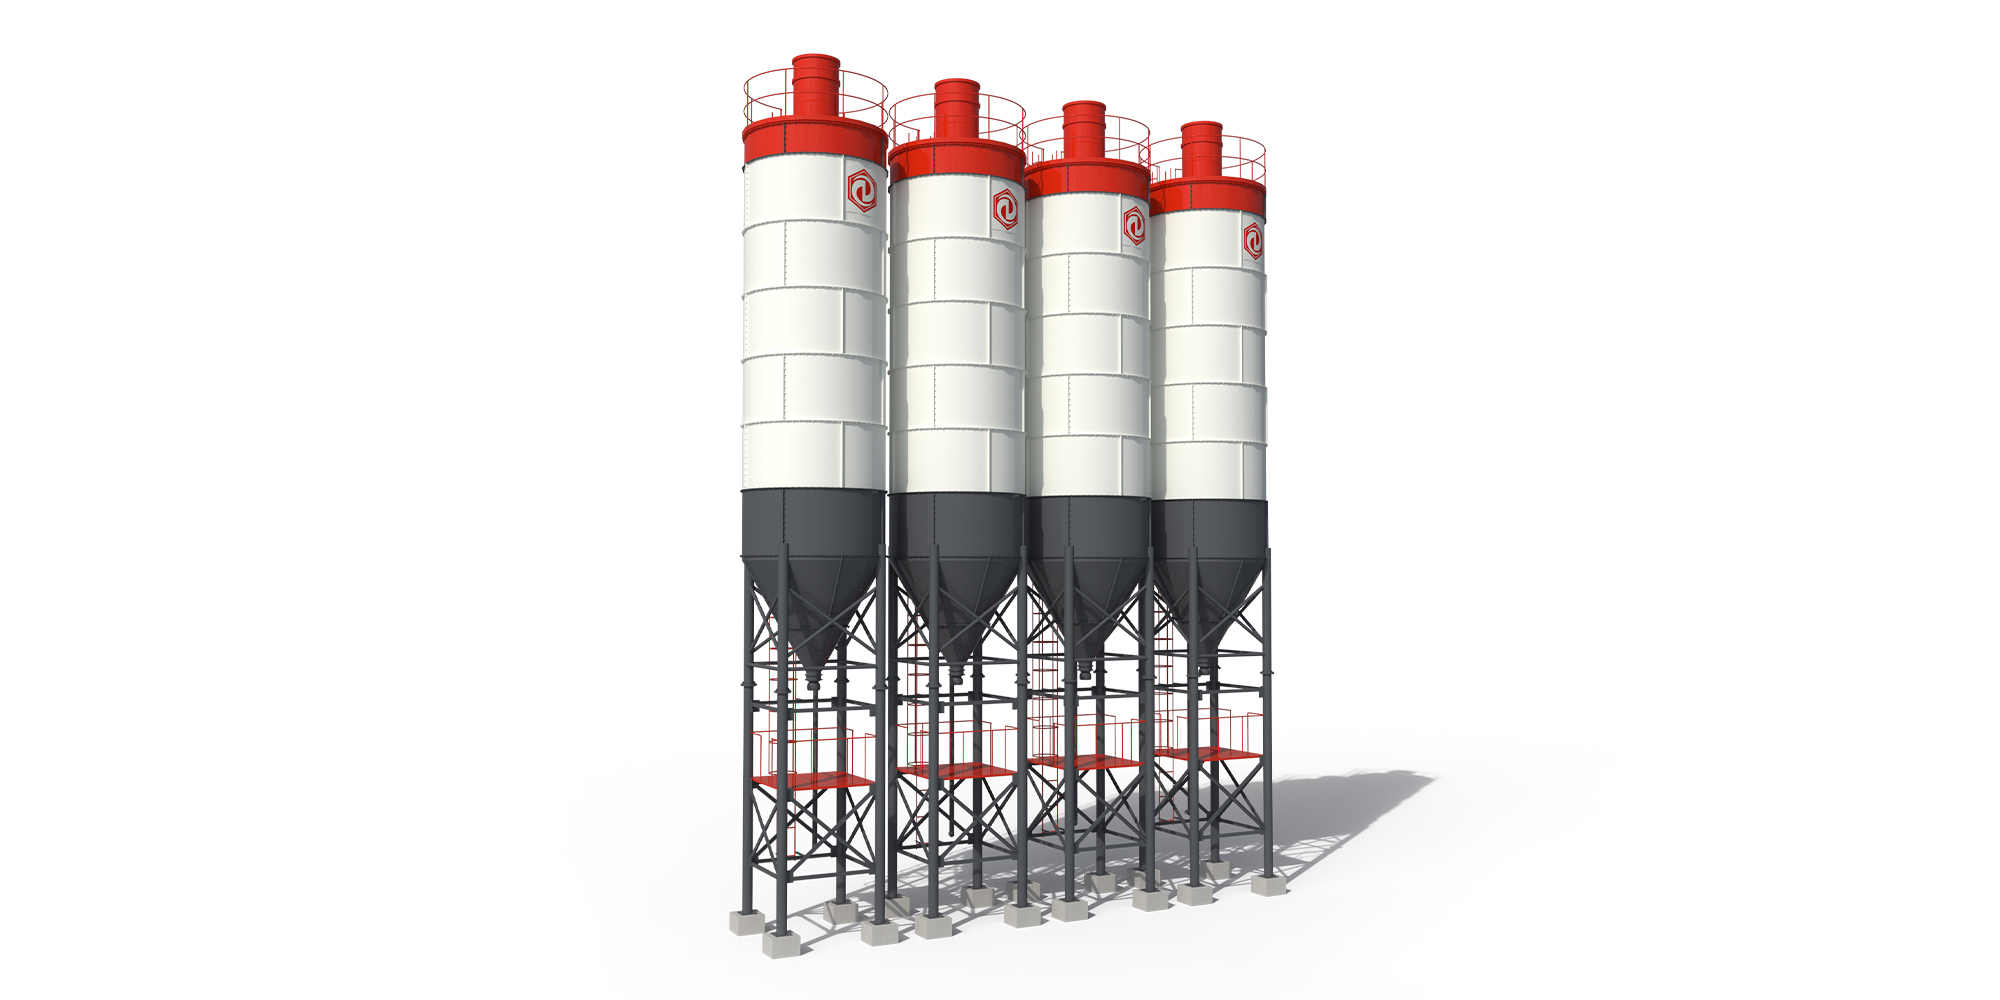 INTERFACE 01 / Cement Silo
Storage and filling locations must coexist with the inclined belt.
Determine usable powder stock and service access together.
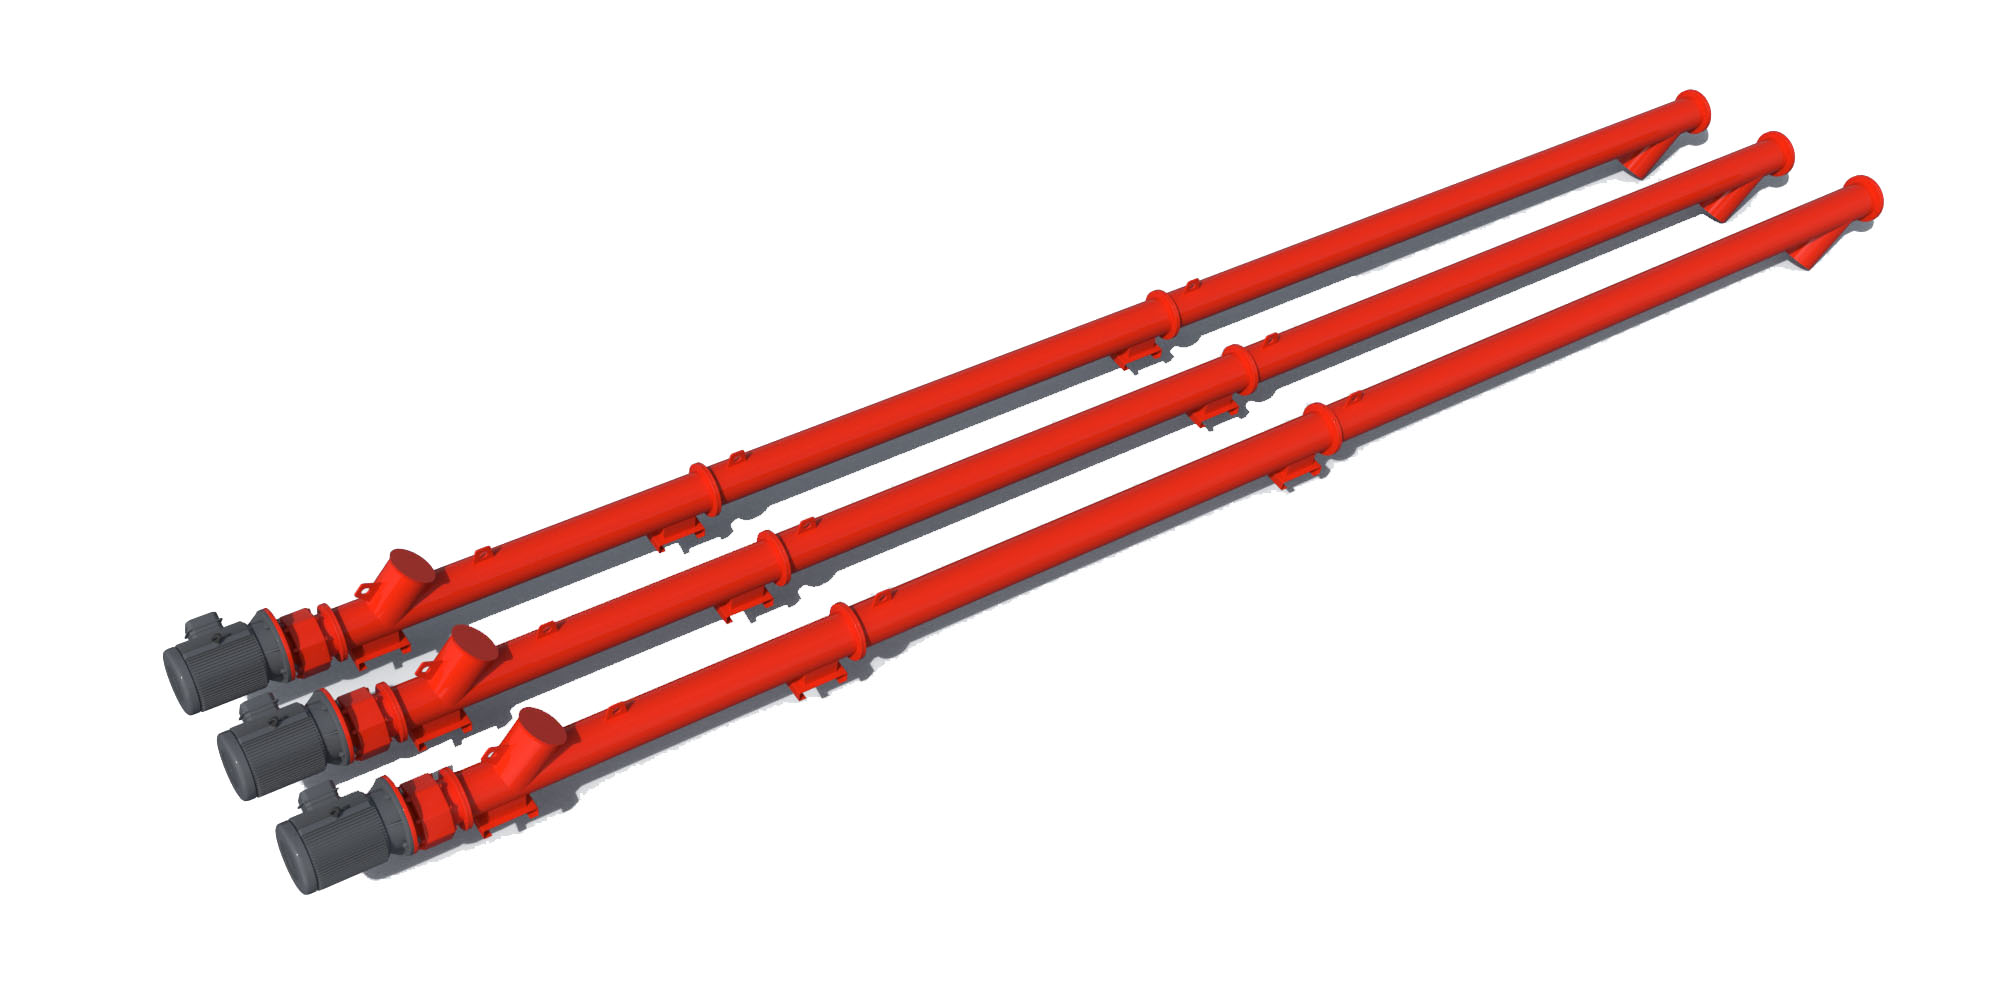 INTERFACE 02 / Screw Conveyor
The cement screw and aggregate belt serve different materials.
Coordinate their separate routes into the weighing and mixing platform.
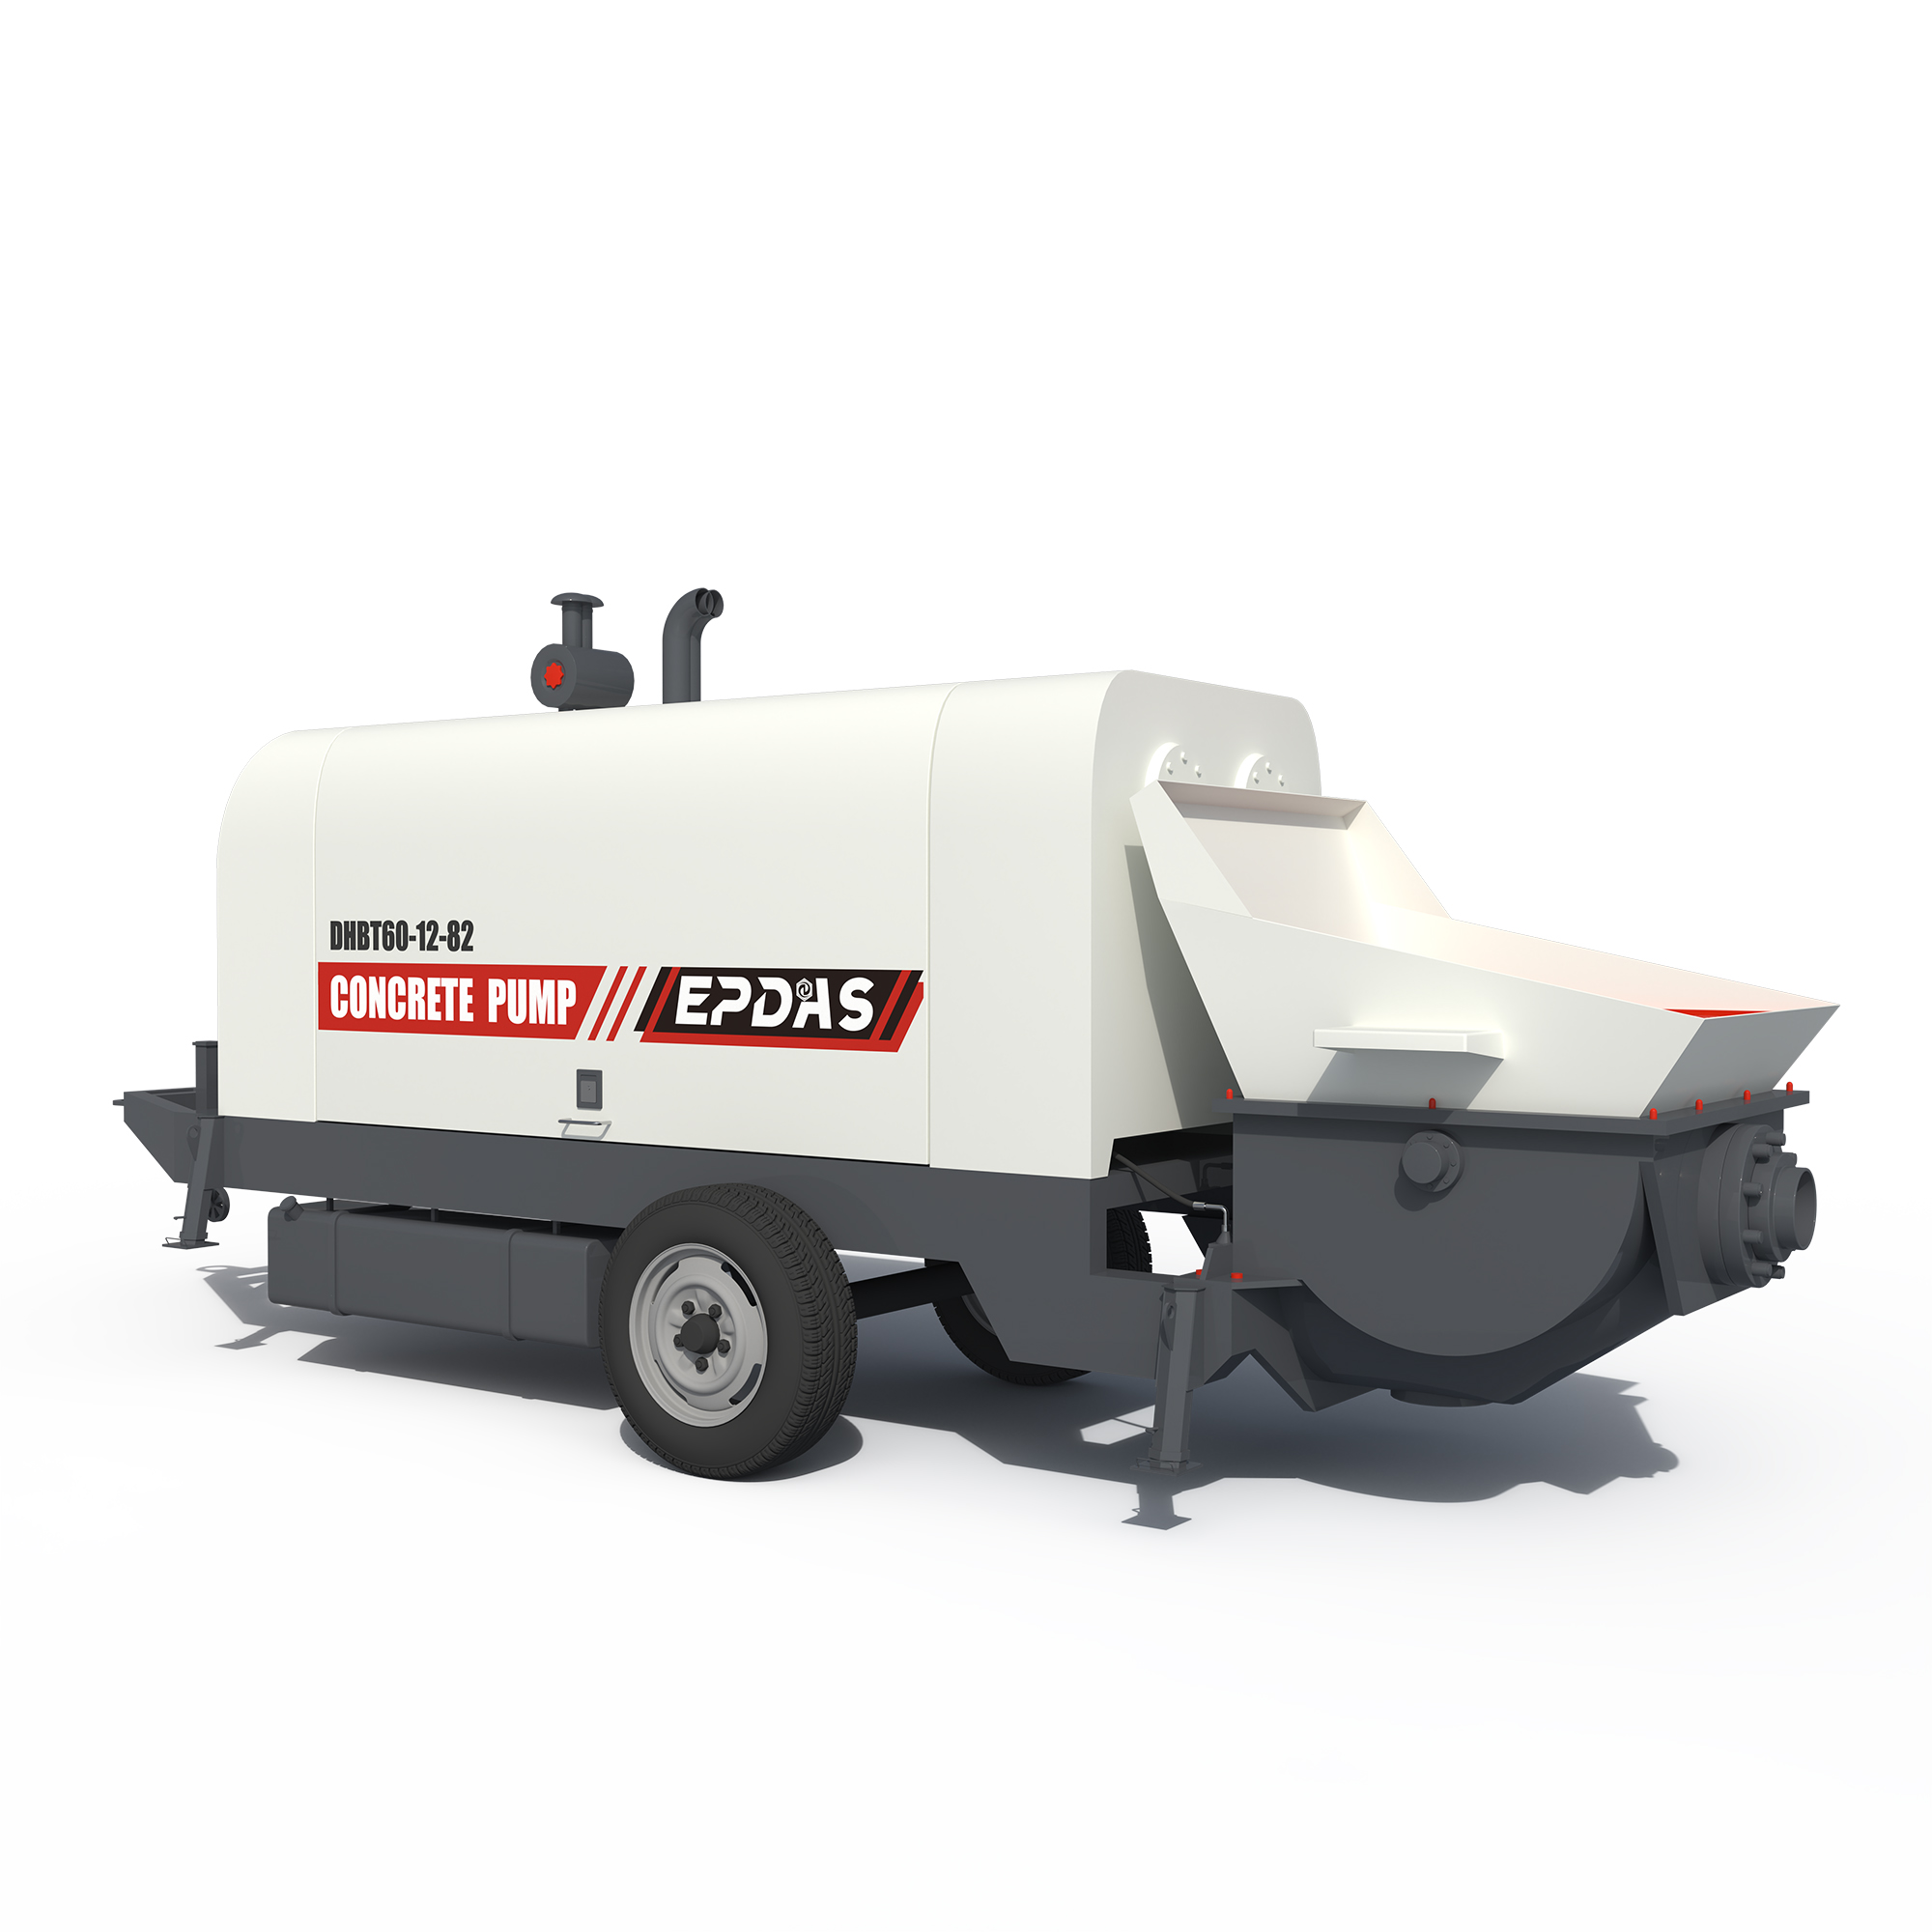 INTERFACE 03 / Trailer Concrete Pump
Pipeline placement requires a concrete receiving stage after this central mixer.
Include supply interruptions in the pump selection discussion.
 INTERFACE 04 / Mobile Concrete Batching Plant
Compare a transportable JS1000 arrangement if future moves are likely.
The stationary belt layout is not itself a relocation package.
Options and alternative architectures are identified in each explanation. This is not a pre-approved matched package. Final connections, duty and supplied components require a model-specific technical review.
Review My Equipment CombinationSeparate the key systems to see what each contributes to the operation.
HZS60 functional separation illustration. Blocks identify subsystem roles; they do not reproduce the machine geometry, assembly sequence or fastening details. Request the approved model drawing for engineering use.
| Parameter | HZS60 |
|---|---|
| Theoretical productivity (m3/hr) | 60 |
| Mixer model | JS1000 |
| Mixing motor power (kw) | 37 |
| Feeding mode | Belt conveyor |
| Cycling period (s) | 60 |
| Max. aggregate size (mm) | Ф80 |
| Aggregate bins capacity (m3) | 3*12 |
| Discharging height (m) | 4.0 |
| Aggregate weighing precision | ±2% |
| Powder weighing precision | ±1% |
| Water weighing precision | ±1% |
| Additive weighing precision | ±1% |
Published EPDAS specifications are a reference for equipment selection. Final specifications and included equipment are confirmed in the quotation.
Original EPDAS Technical Reference ↗| Selection reference | HZS60 · This model | HZS90 | HZS120 |
|---|---|---|---|
| Theoretical productivity (m3/hr) | 60 | 90 | 120 |
| Mixer model | JS1000 | JS1500 | JS2000 |
| Feeding mode | Belt conveyor | Belt conveyor | Belt conveyor |
| Aggregate bins capacity (m3) | 3*12 | 3*12 | 4*20 |
| Discharging height (m) | 4.0 | 4.0 | 4.0 |
Review HZS60 when a dedicated site is being designed around conveyor-fed aggregate delivery.
Mixer model: JS1000
Mixing motor power (kw): 37
Aggregate bins capacity (m3): 3*12
Confirm core equipment, options, buyer-provided systems, transport modules, inspection documents and support responsibilities in the quotation.